FabVitals Planning
Plan against real capacity. Follow every order as it happens.
AI-driven scheduling by work centre, production declared at the station, and material that reaches the line before the line needs it — one system, from the plan to the finished lot.
Today
The plan is a spreadsheet that is out of date by mid-morning, progress arrives on paper the next day, and nobody knows whether the material for the next order is already at the line.
After
Every order shows its real step, quantity and delay as it happens, material moves to the work centre on request, and the planner re-sequences from facts.
What changes
Three things that change on the floor.
A plan the floor can follow
Sequenced with finite capacity by work centre, regenerated whenever an order changes, and adjusted by hand where the planner knows better.
Progress recorded at source
Each station opens a session for its order and step and declares what it produced, so the state of every order is current without anyone typing it in later.
Material under control
Requisitions to the work centre, stock by location and lot, and every movement recorded — the line does not stop waiting for material nobody knew was missing.
The product at work
From the plan to the finished lot.
Real screens of FabVitals, in the order information flows through the factory.
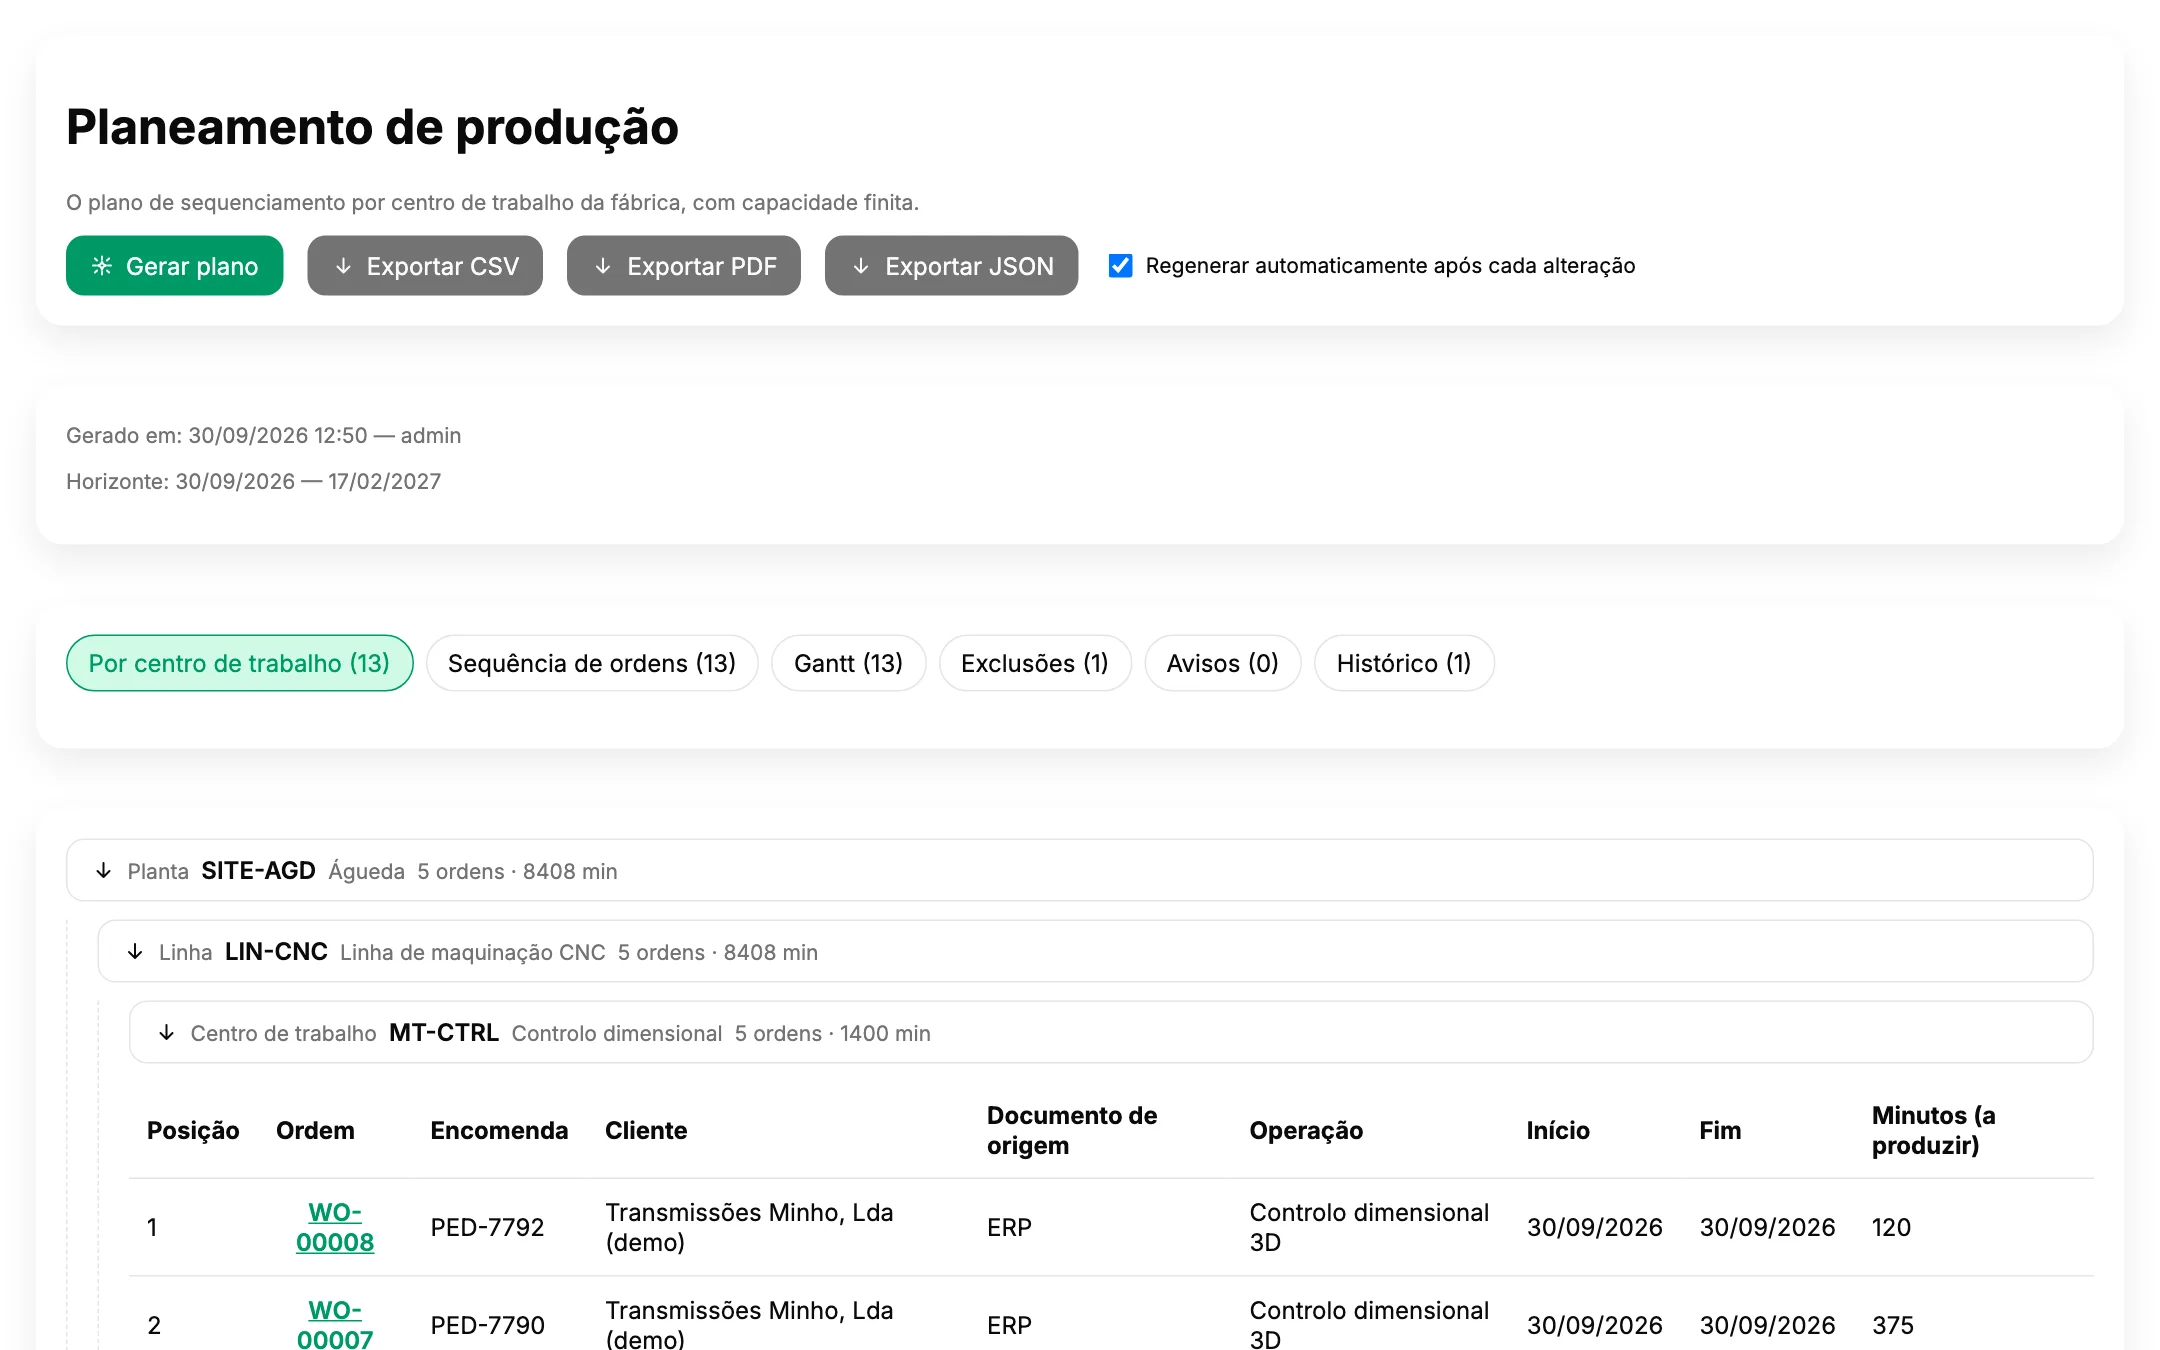
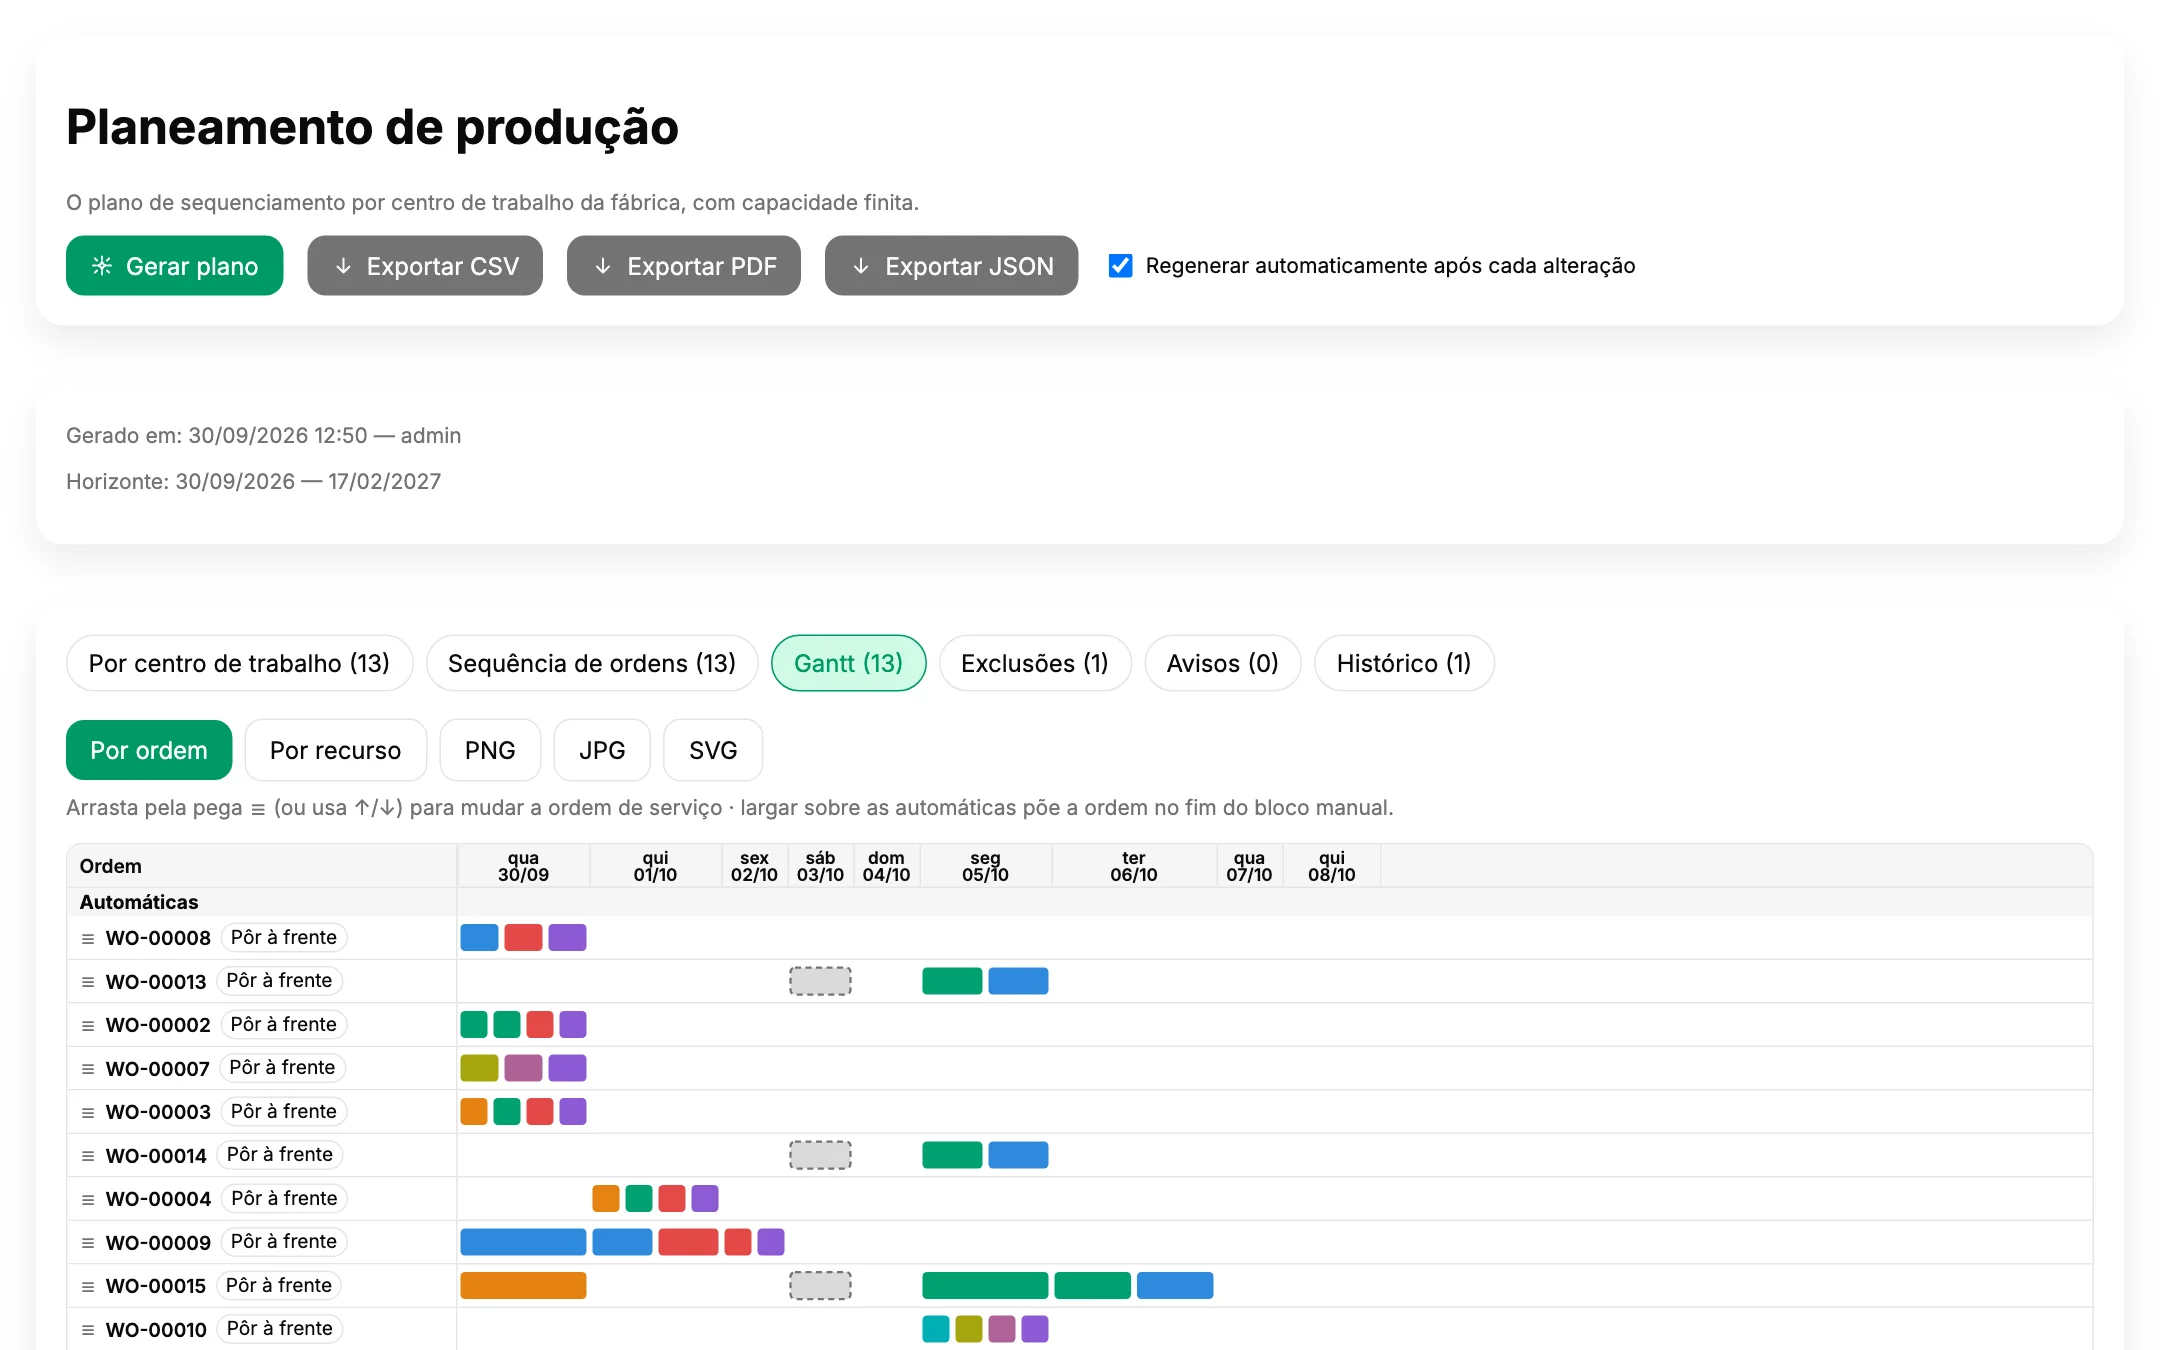
Production planning
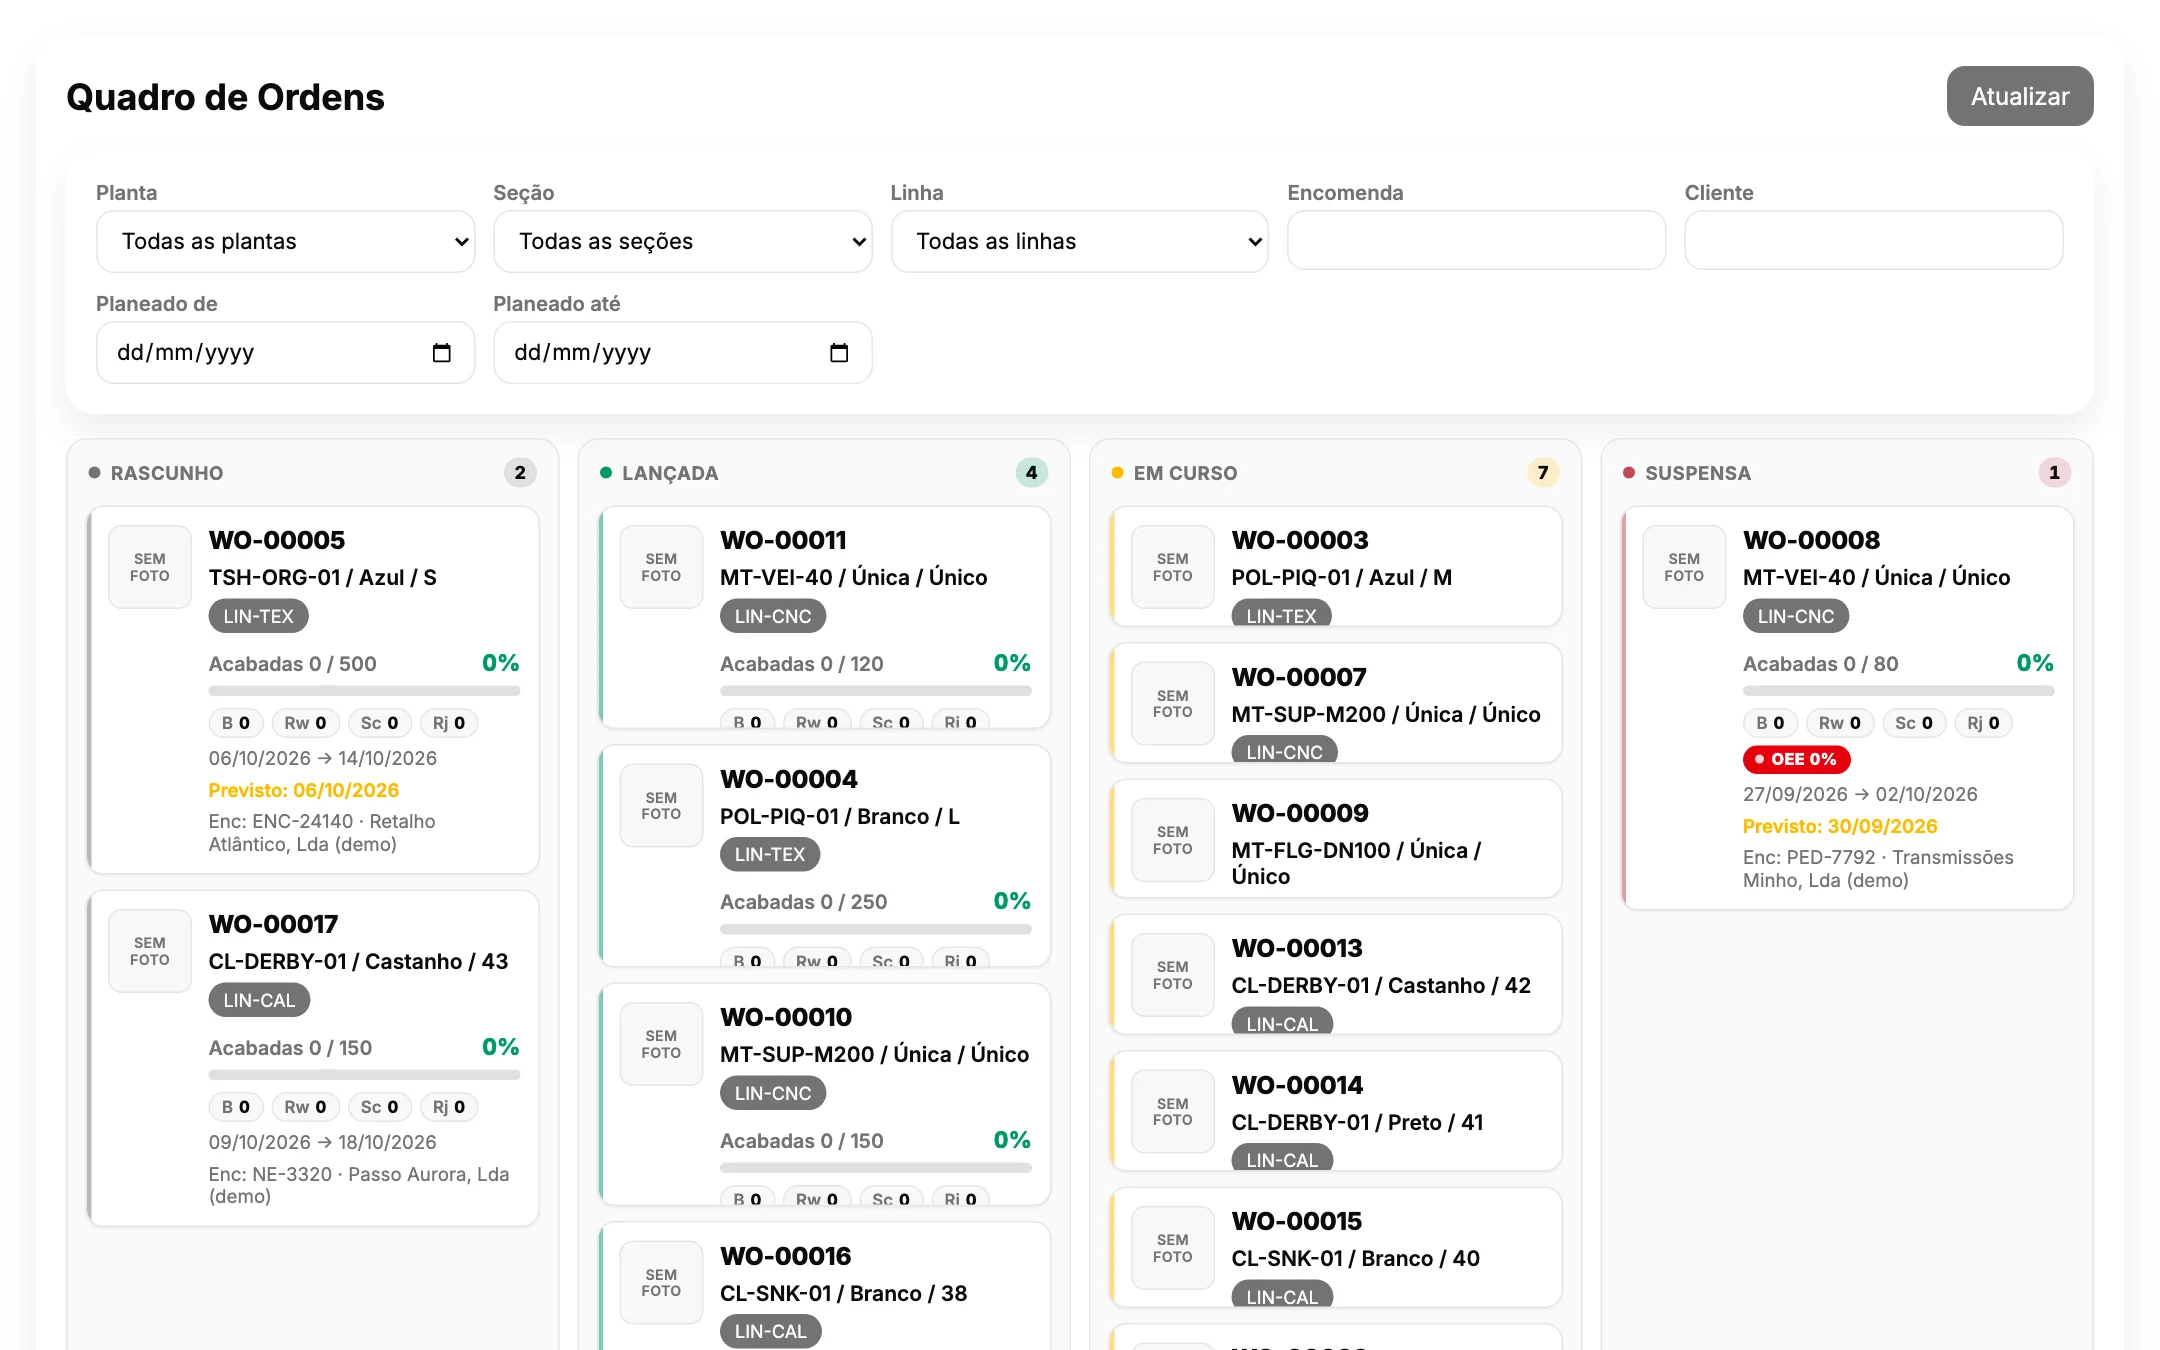
The plan is generated with finite capacity for each work centre and can be regenerated after every change. The board shows every order by state.
Tracking each article through production
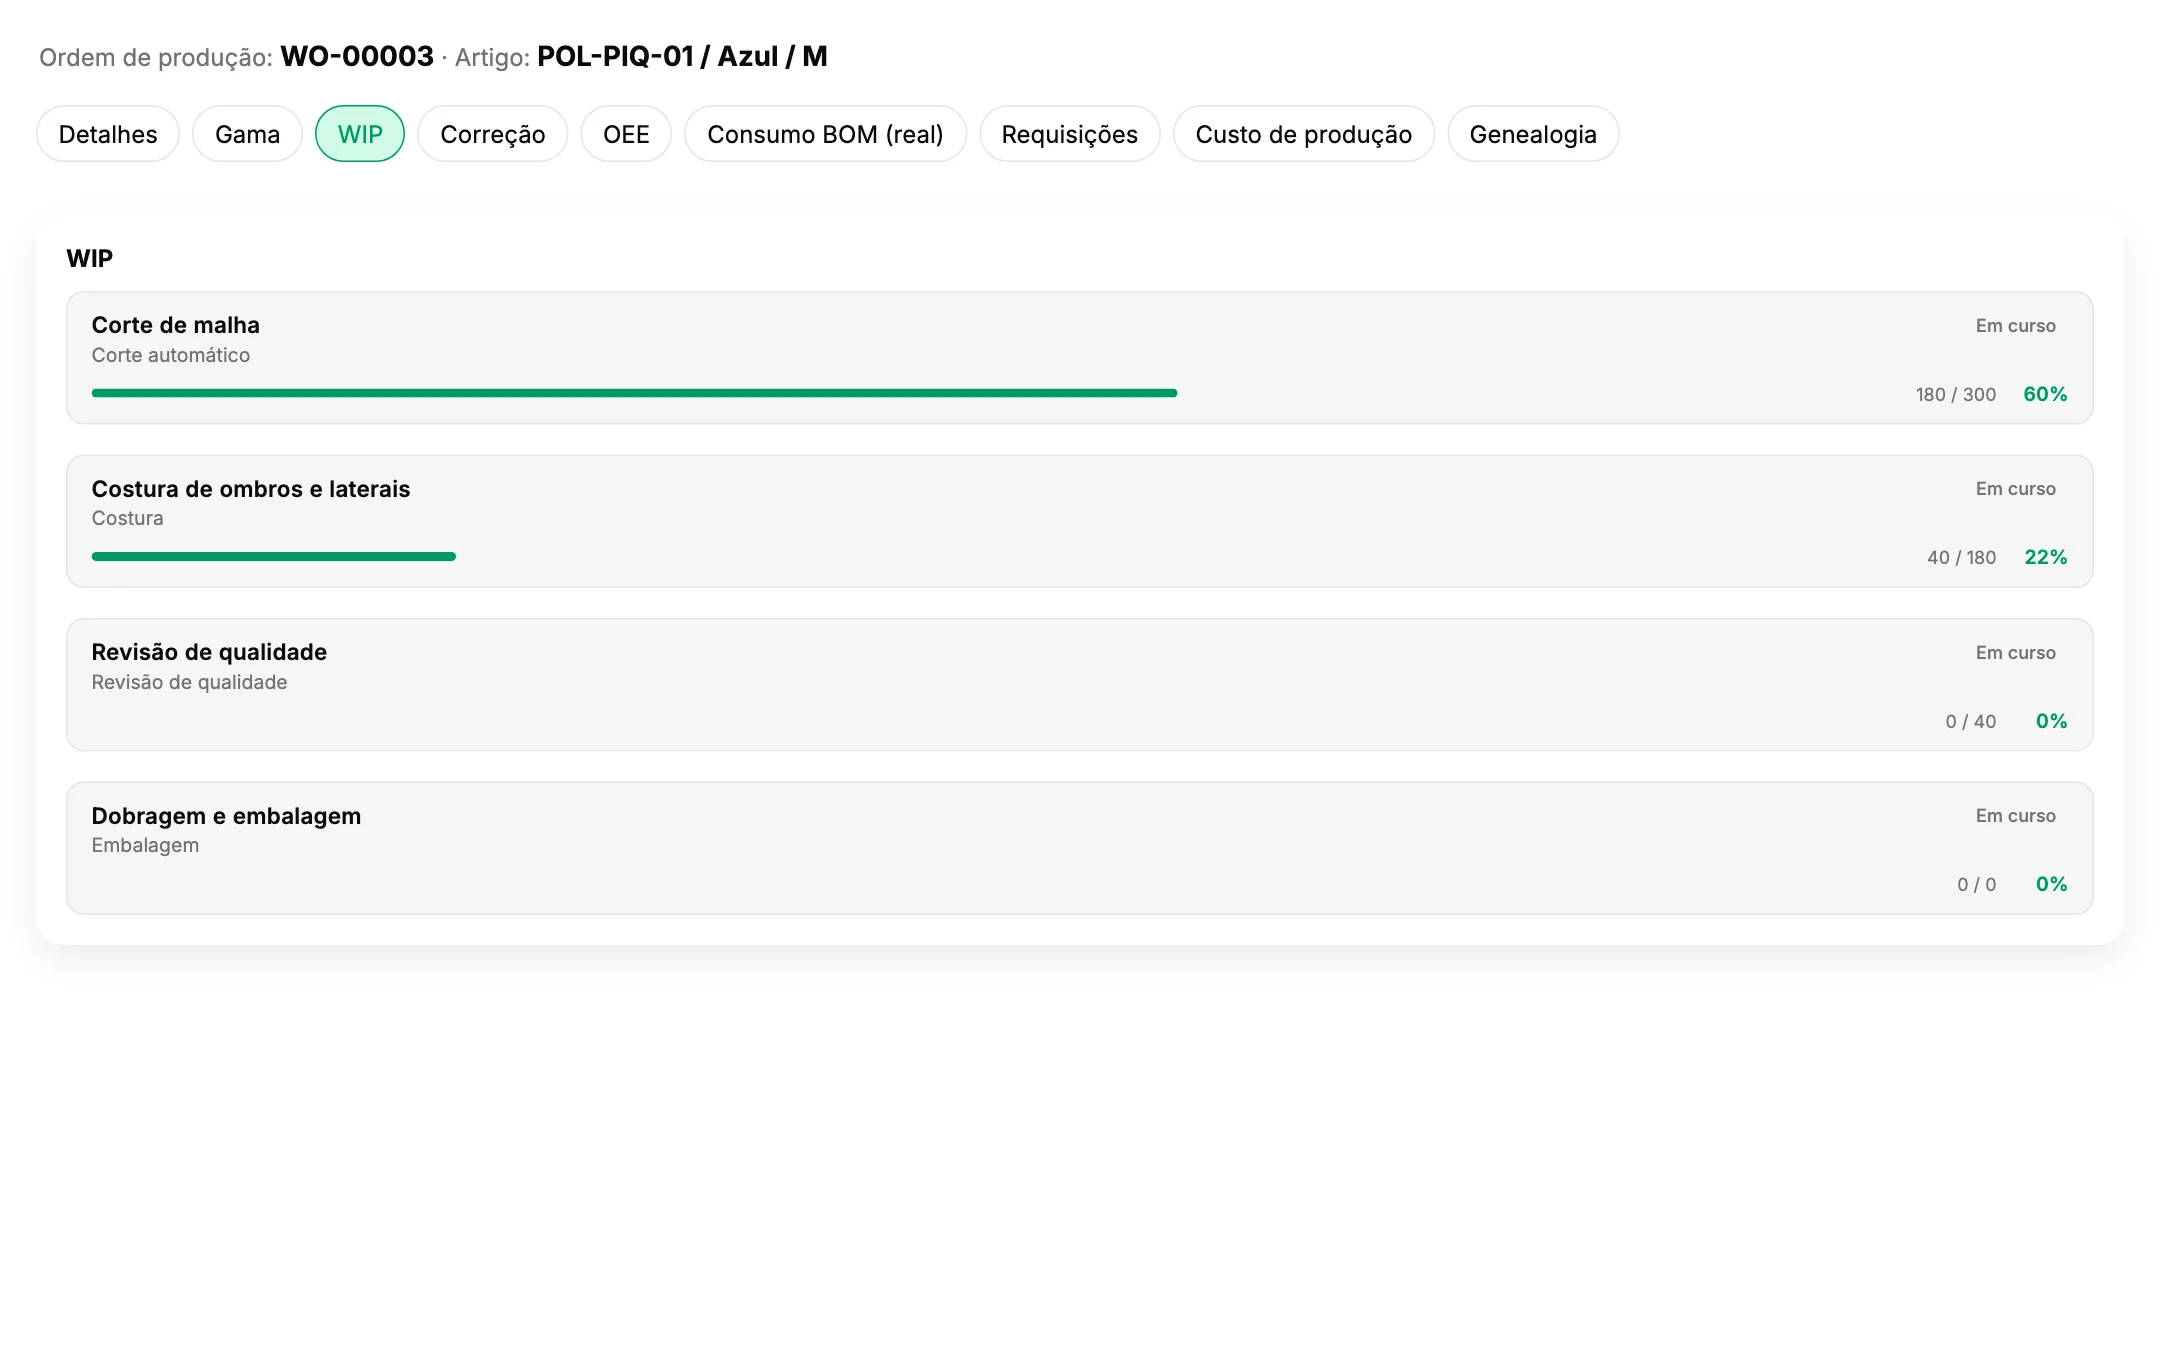
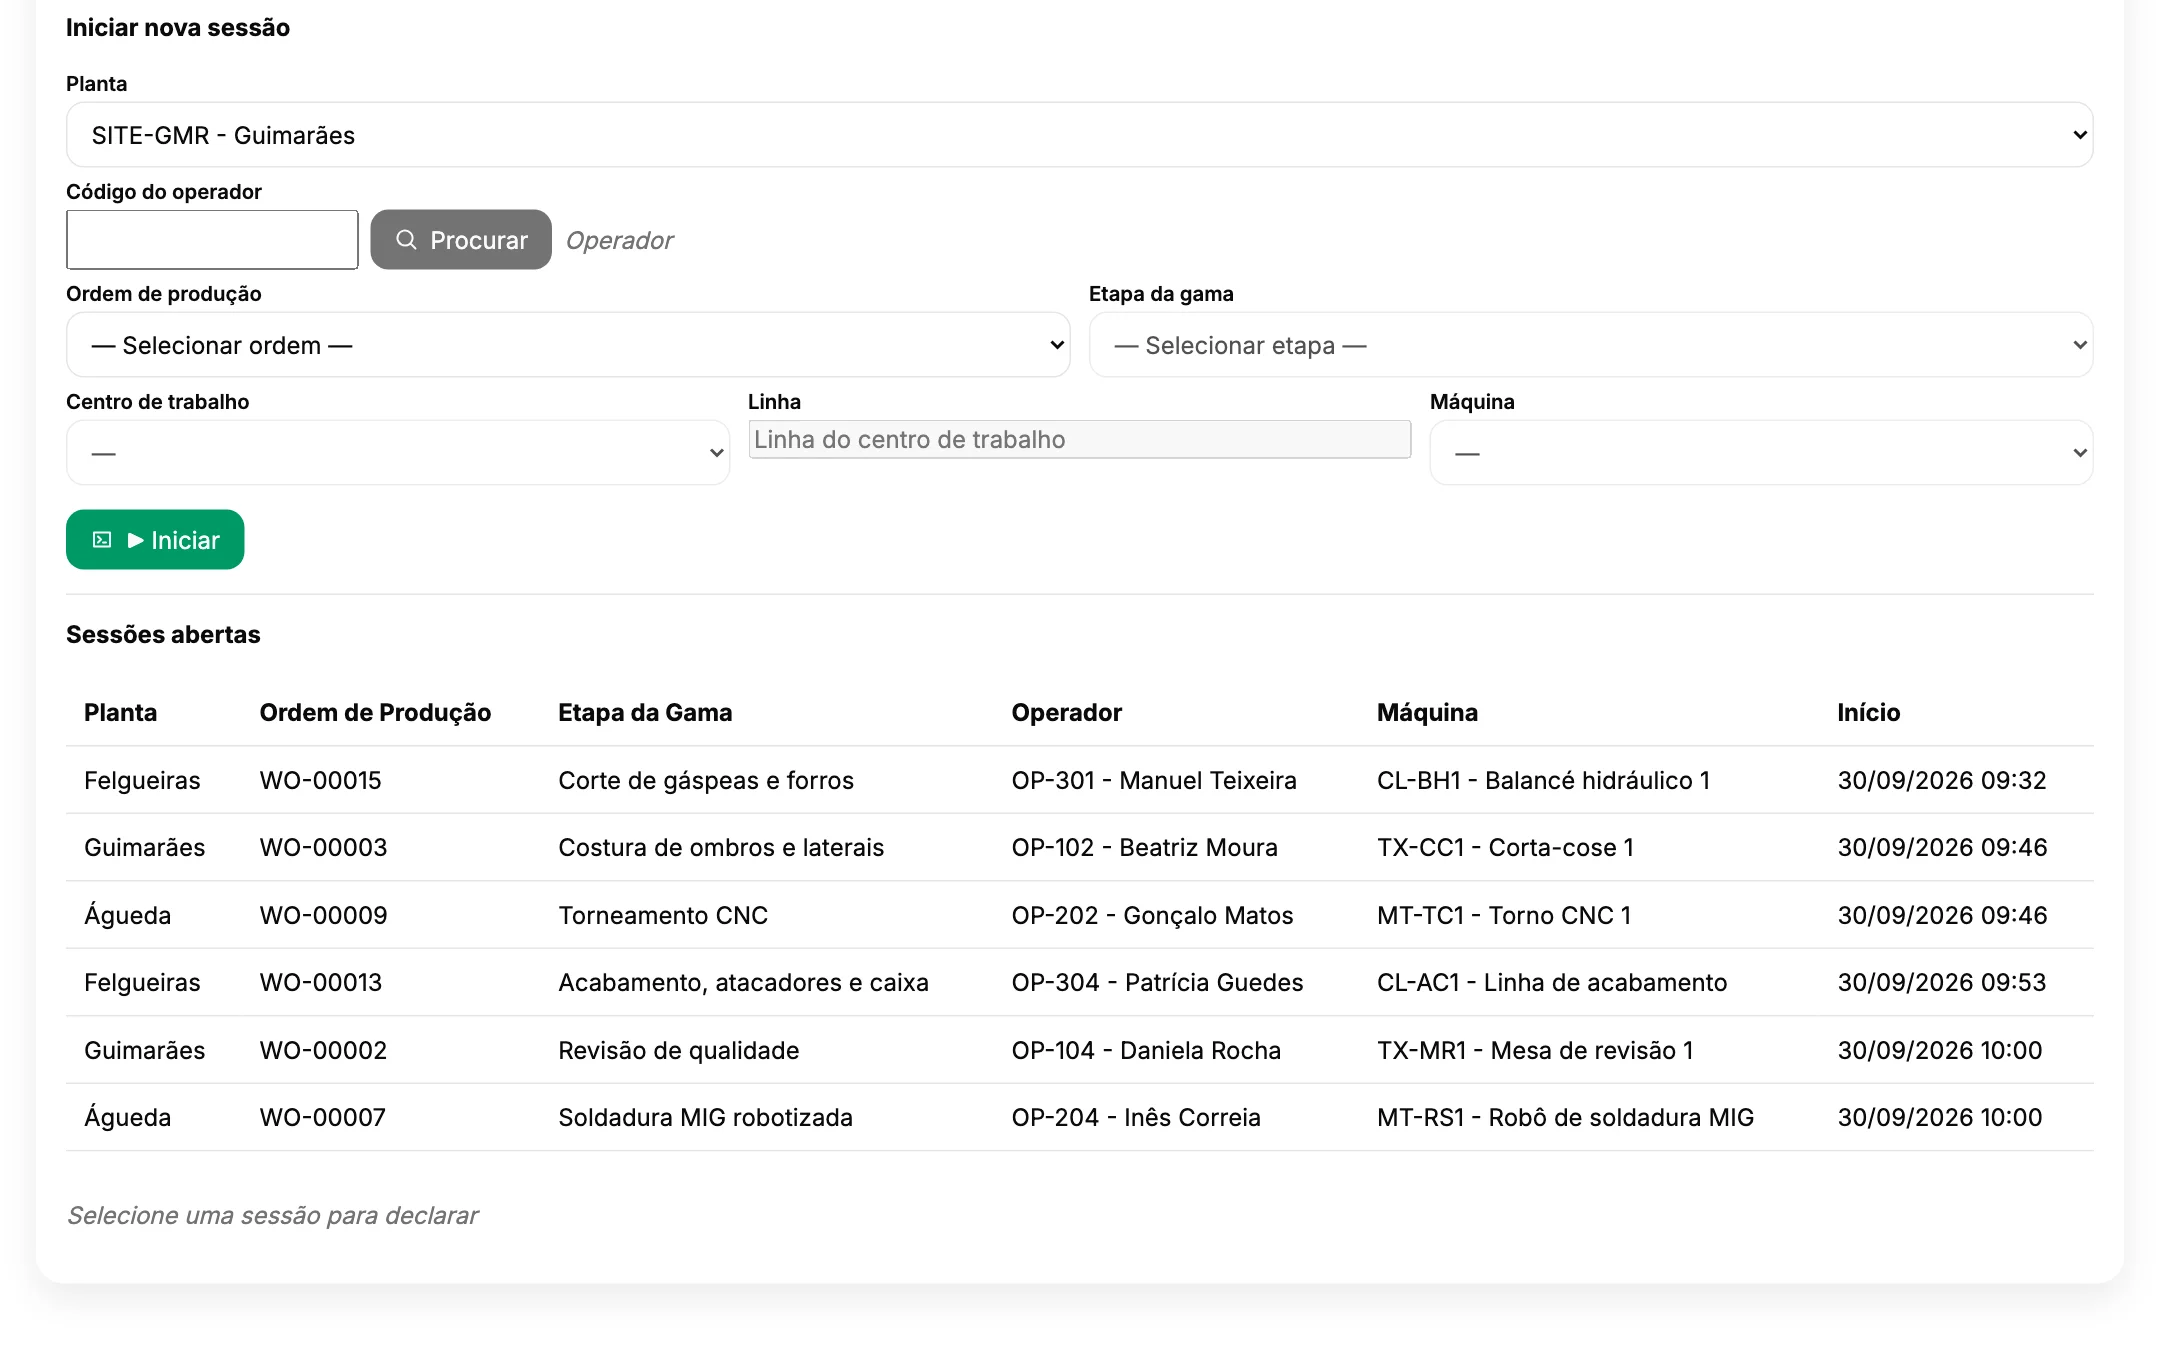
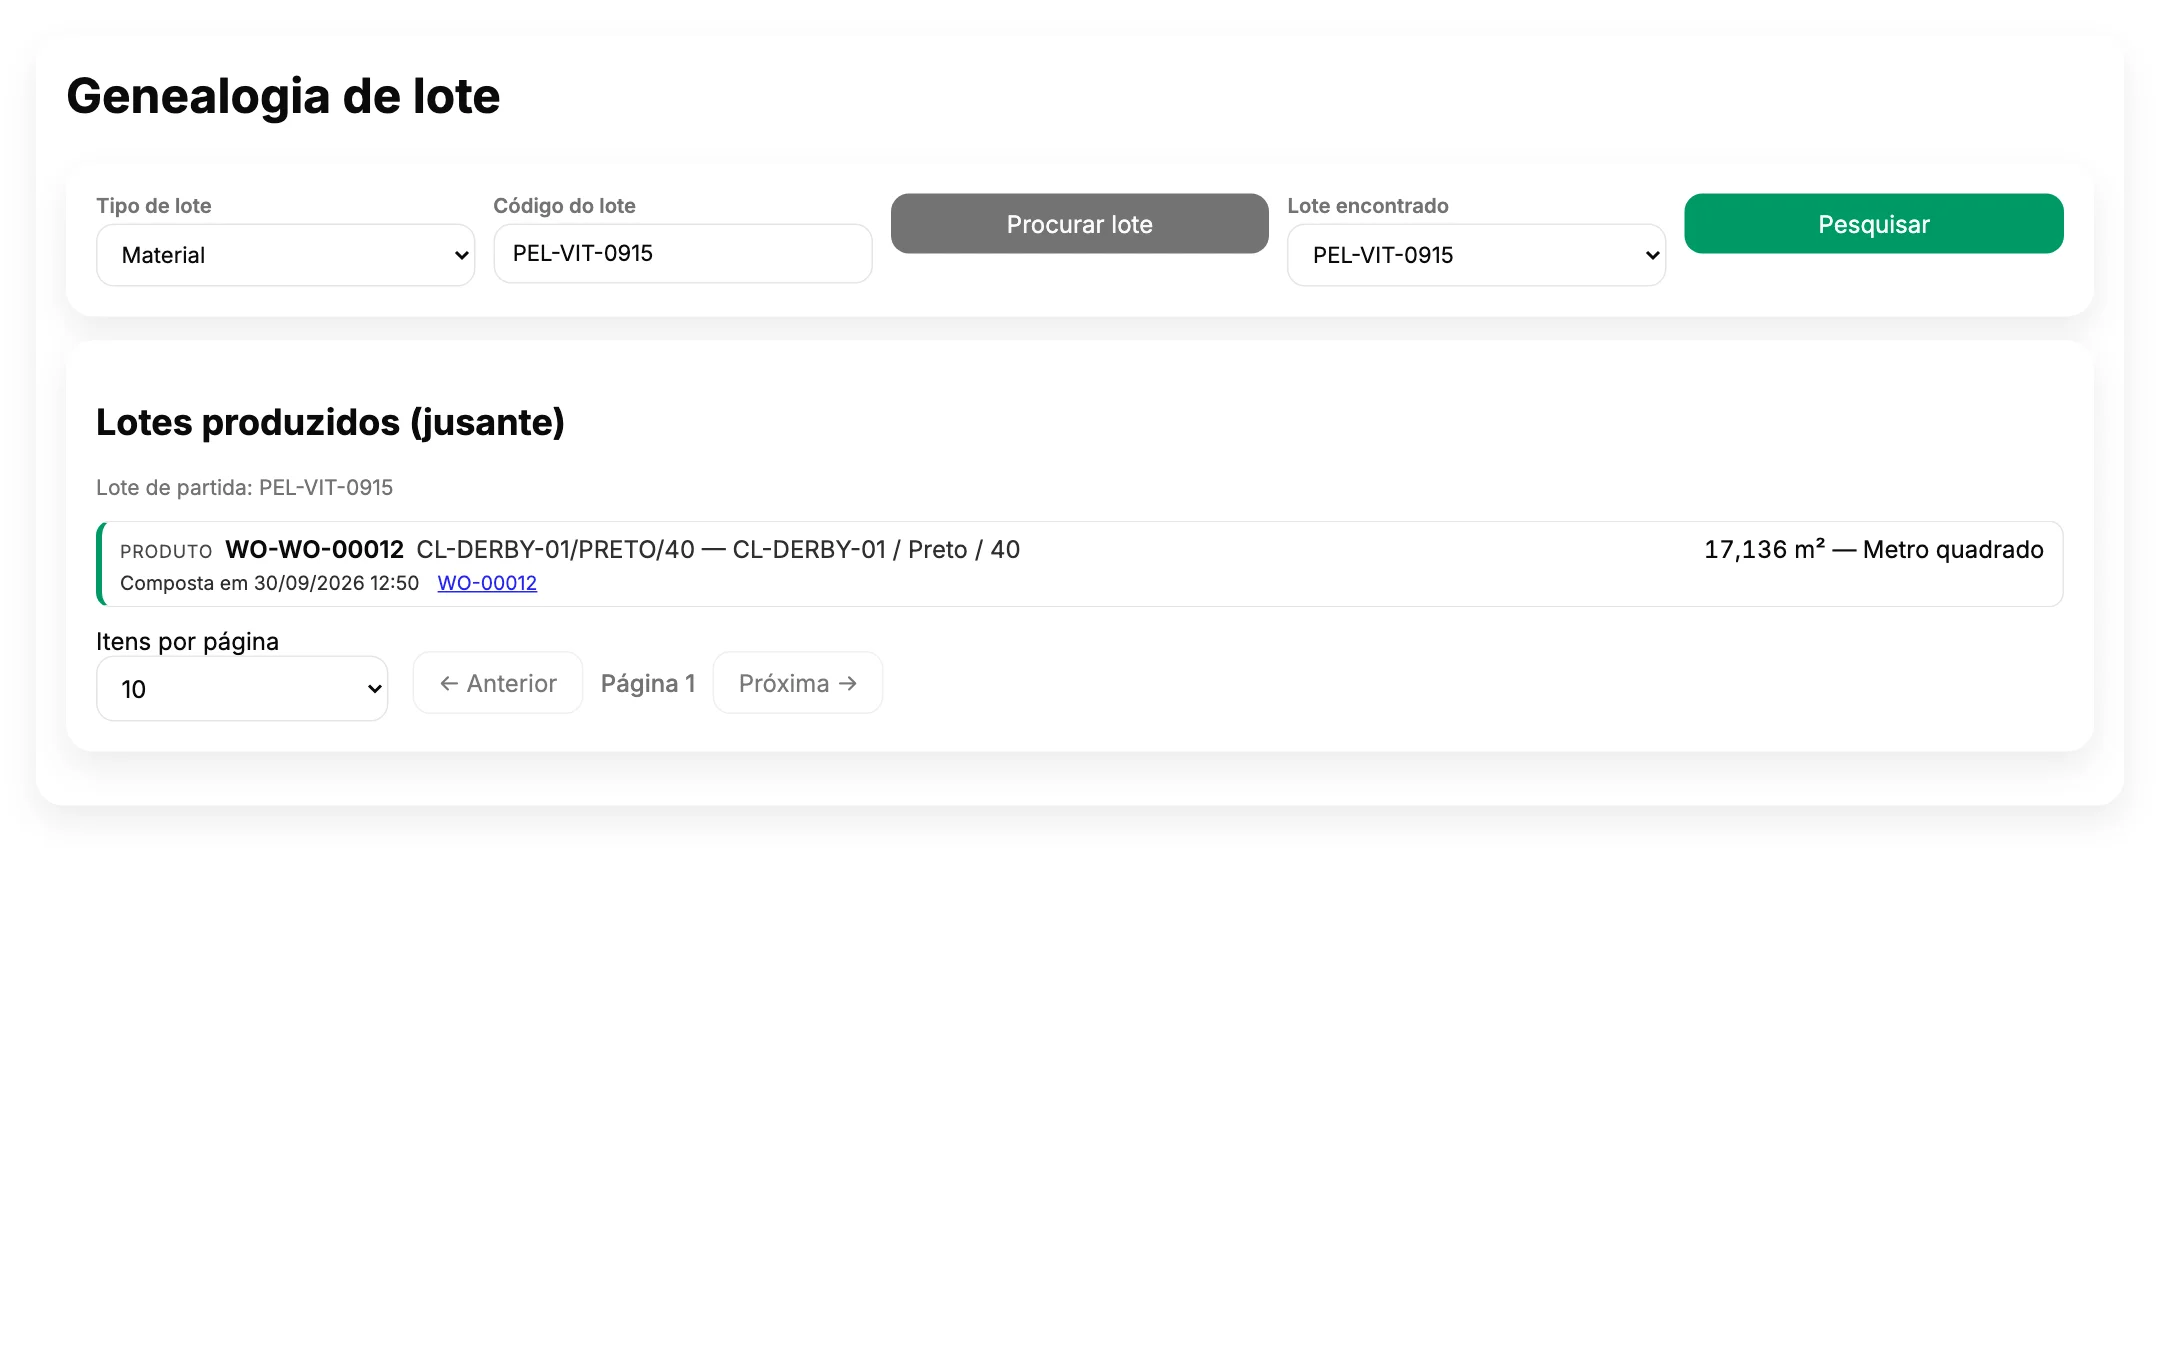
Each order shows how far every step of its routing has gone. Operators declare production against their session, and each lot can be traced back to its materials.
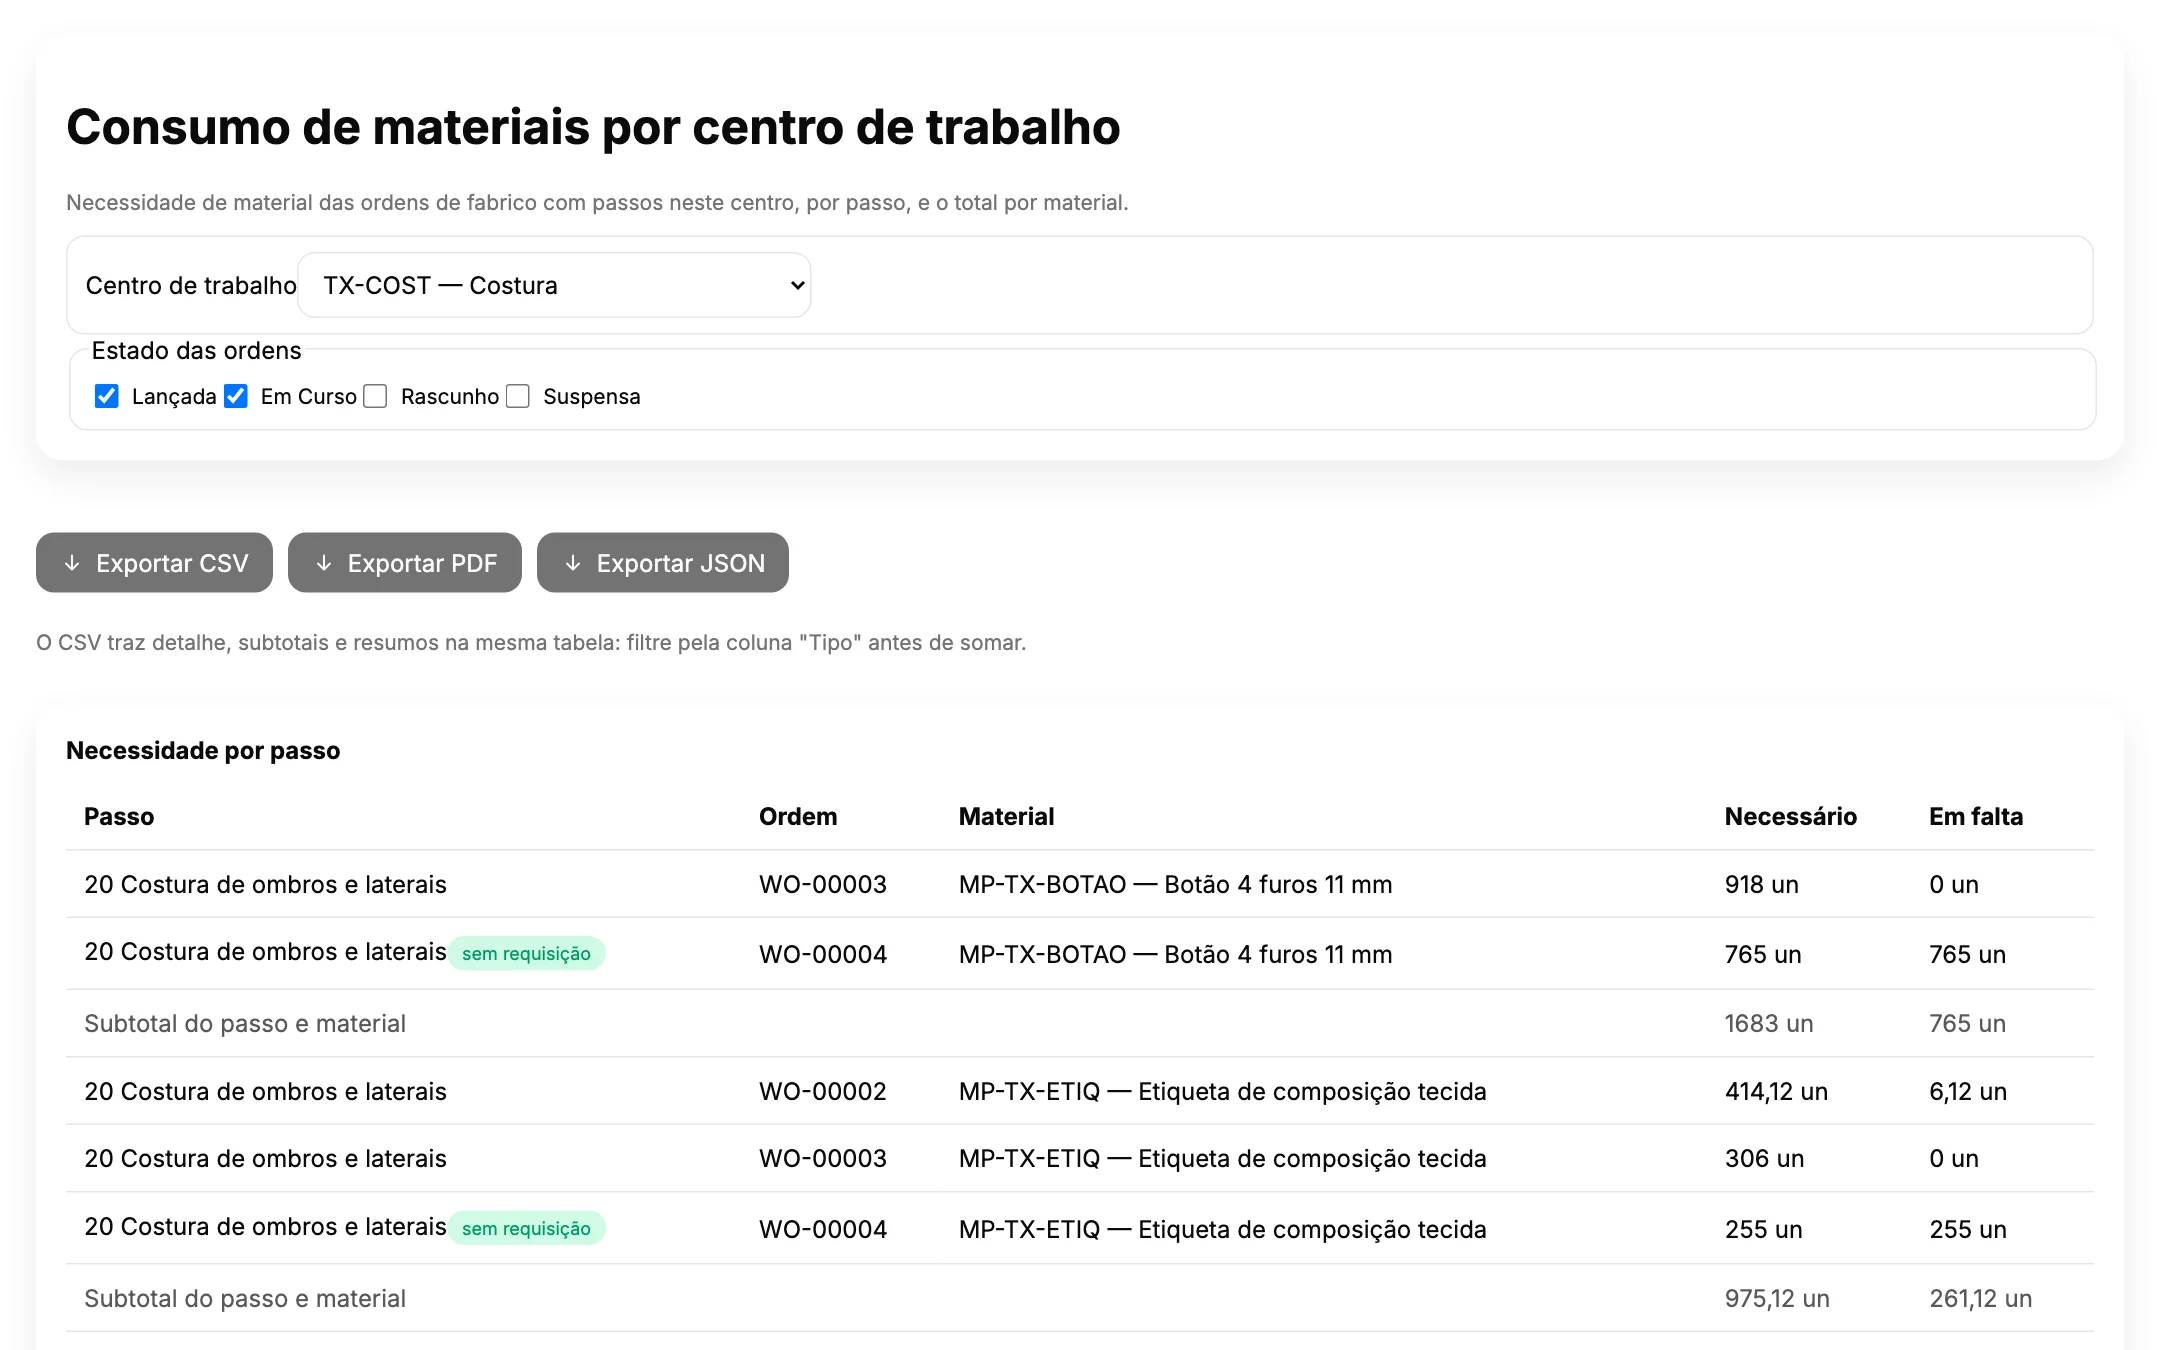
Moving material to the work centre
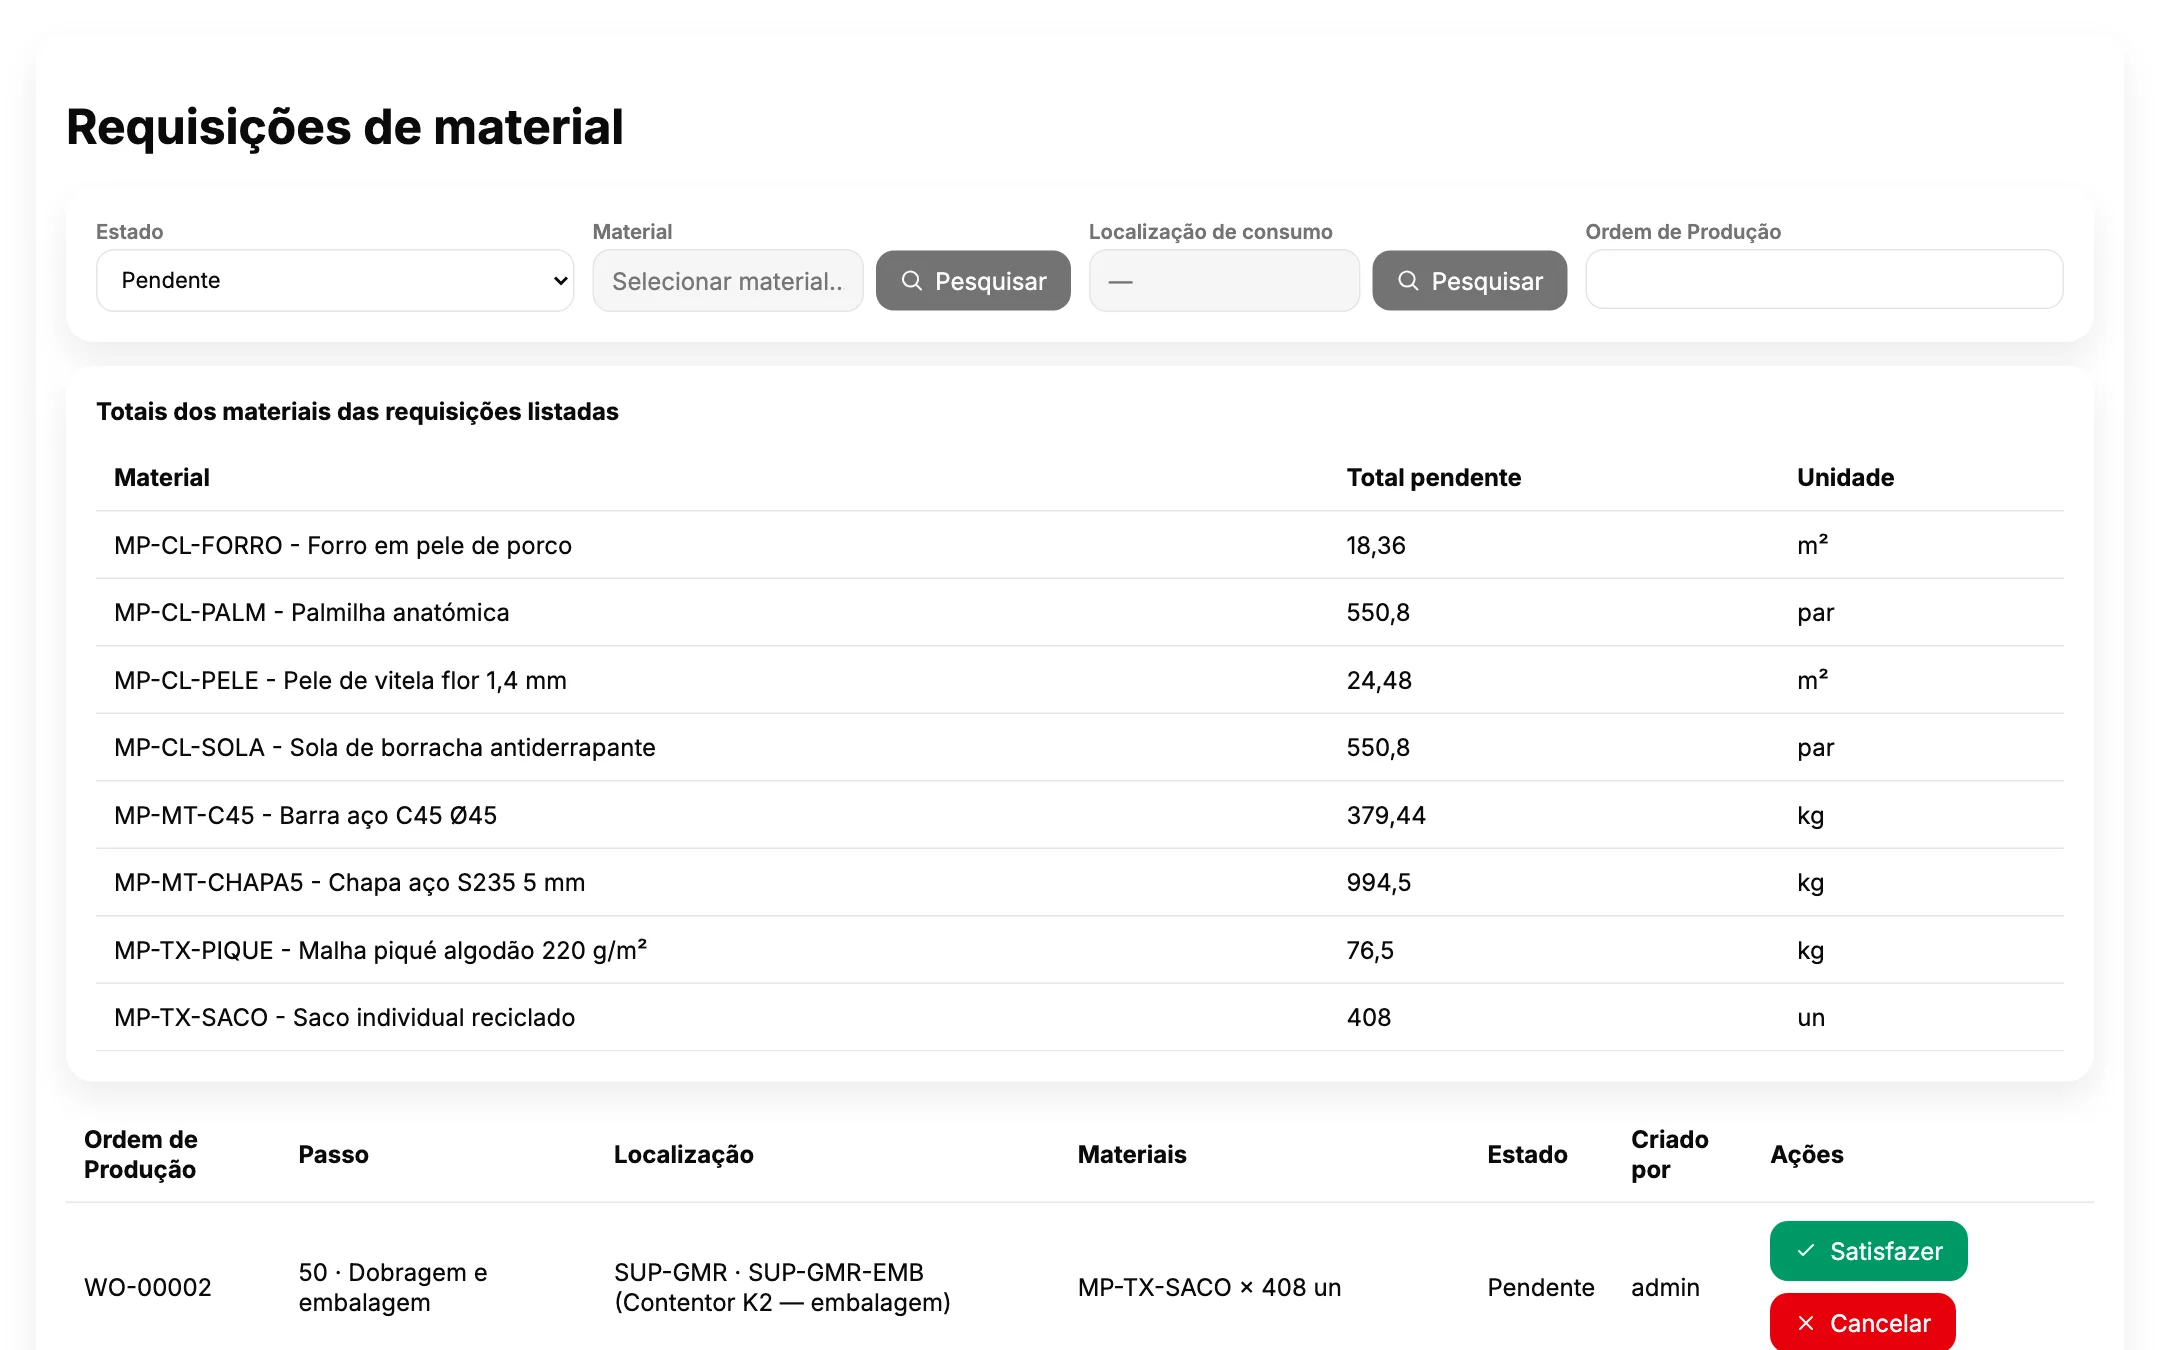
Material is requested for the step that will consume it and delivered to the location at the line. Each work centre sees what its orders need and what is still missing.
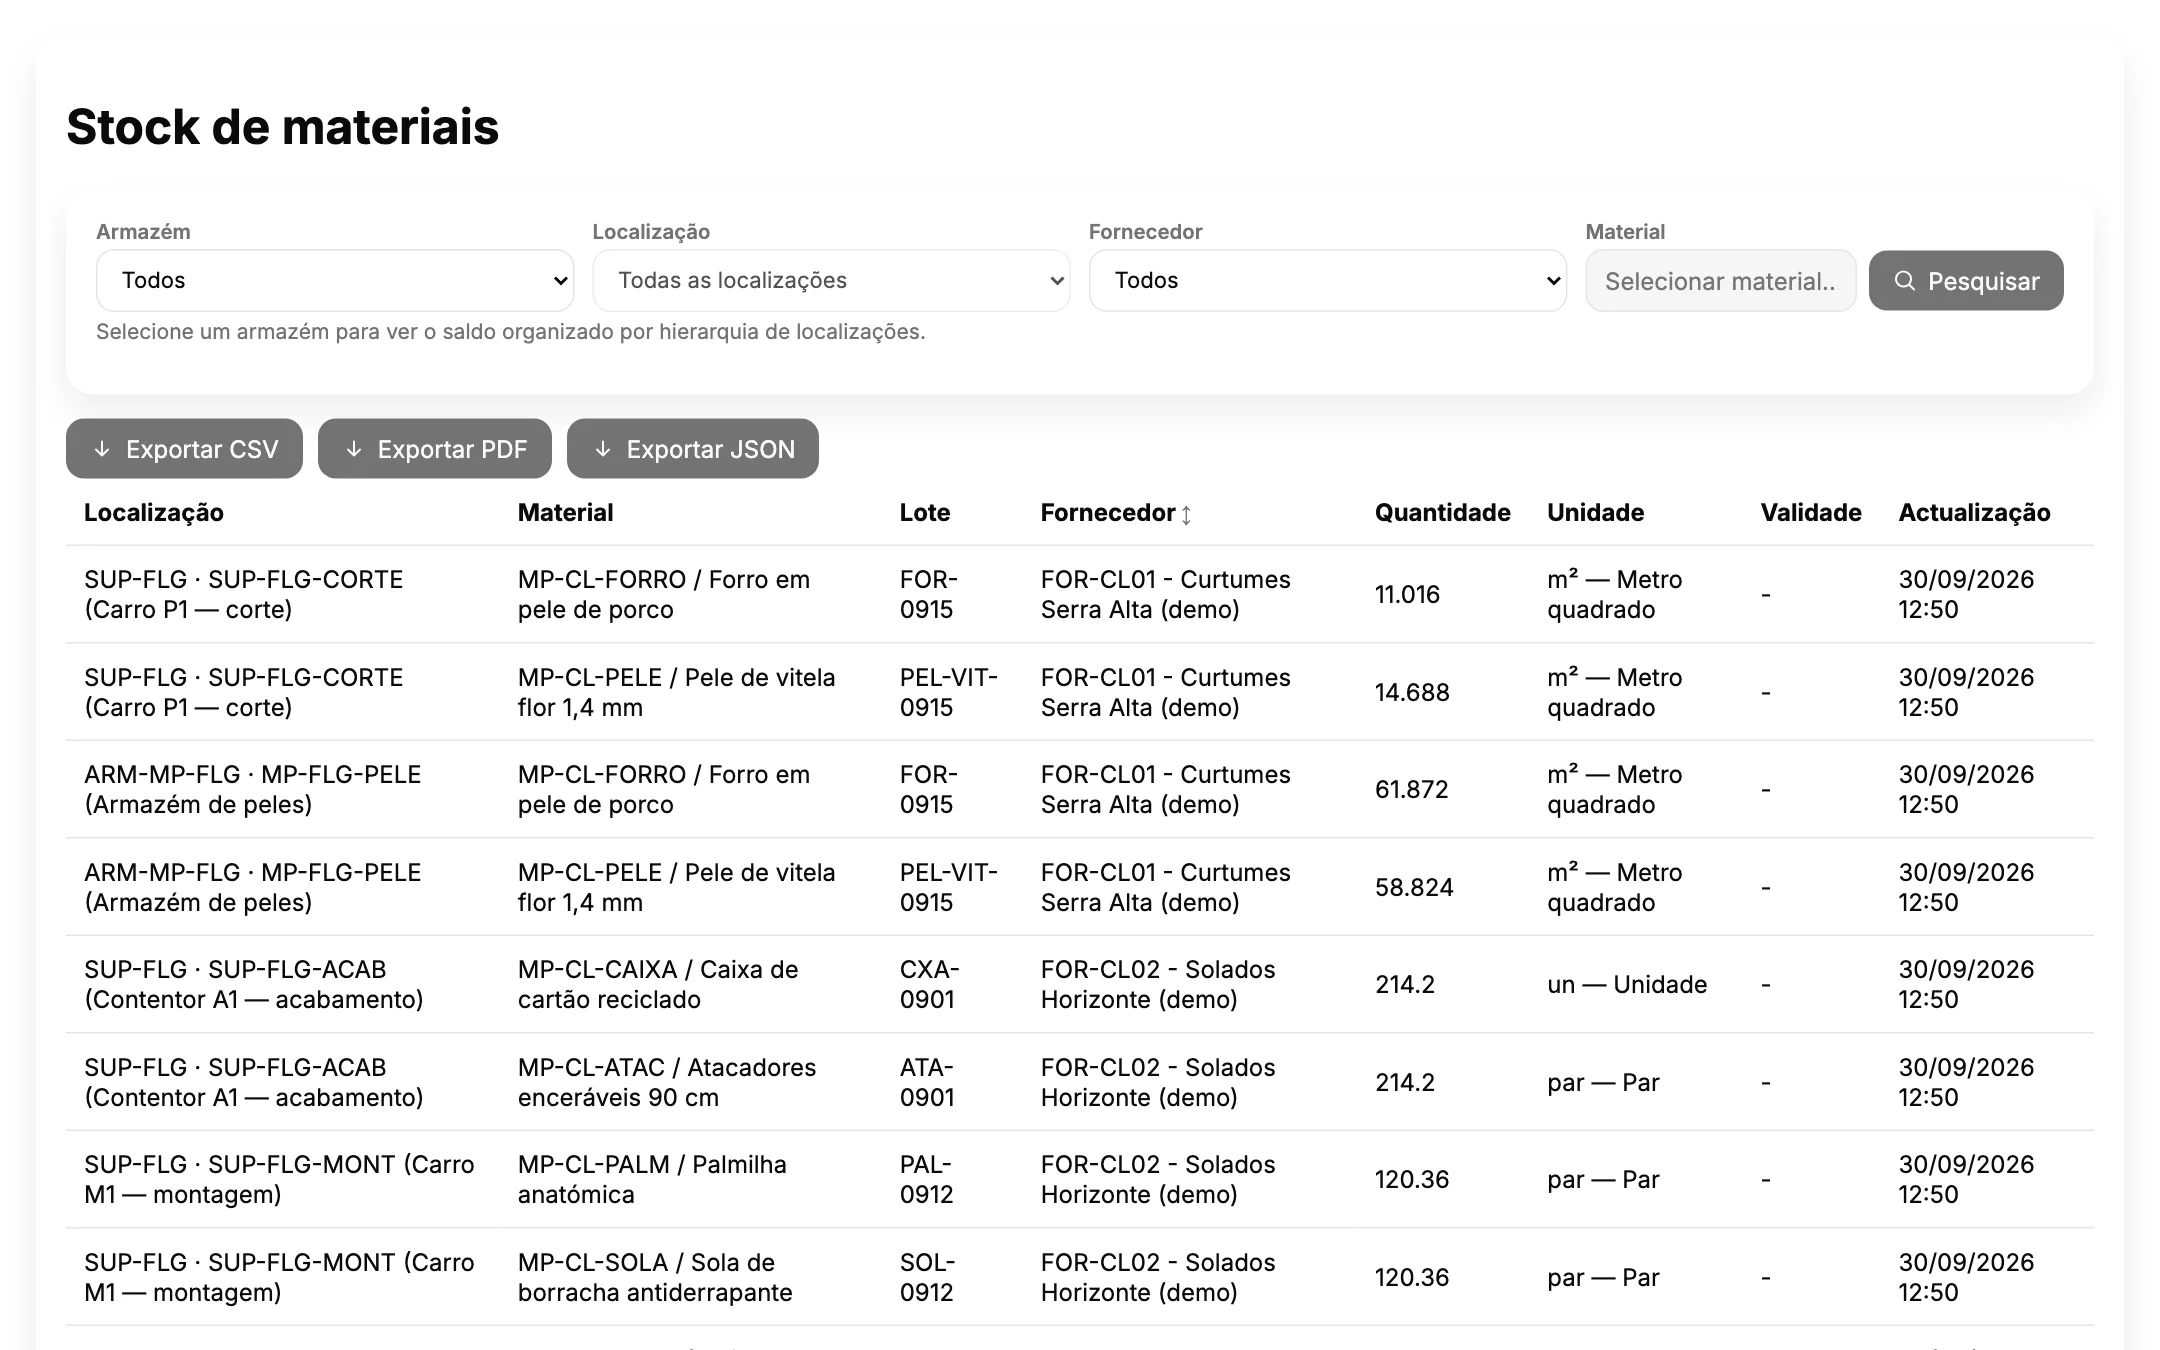
Raw material control
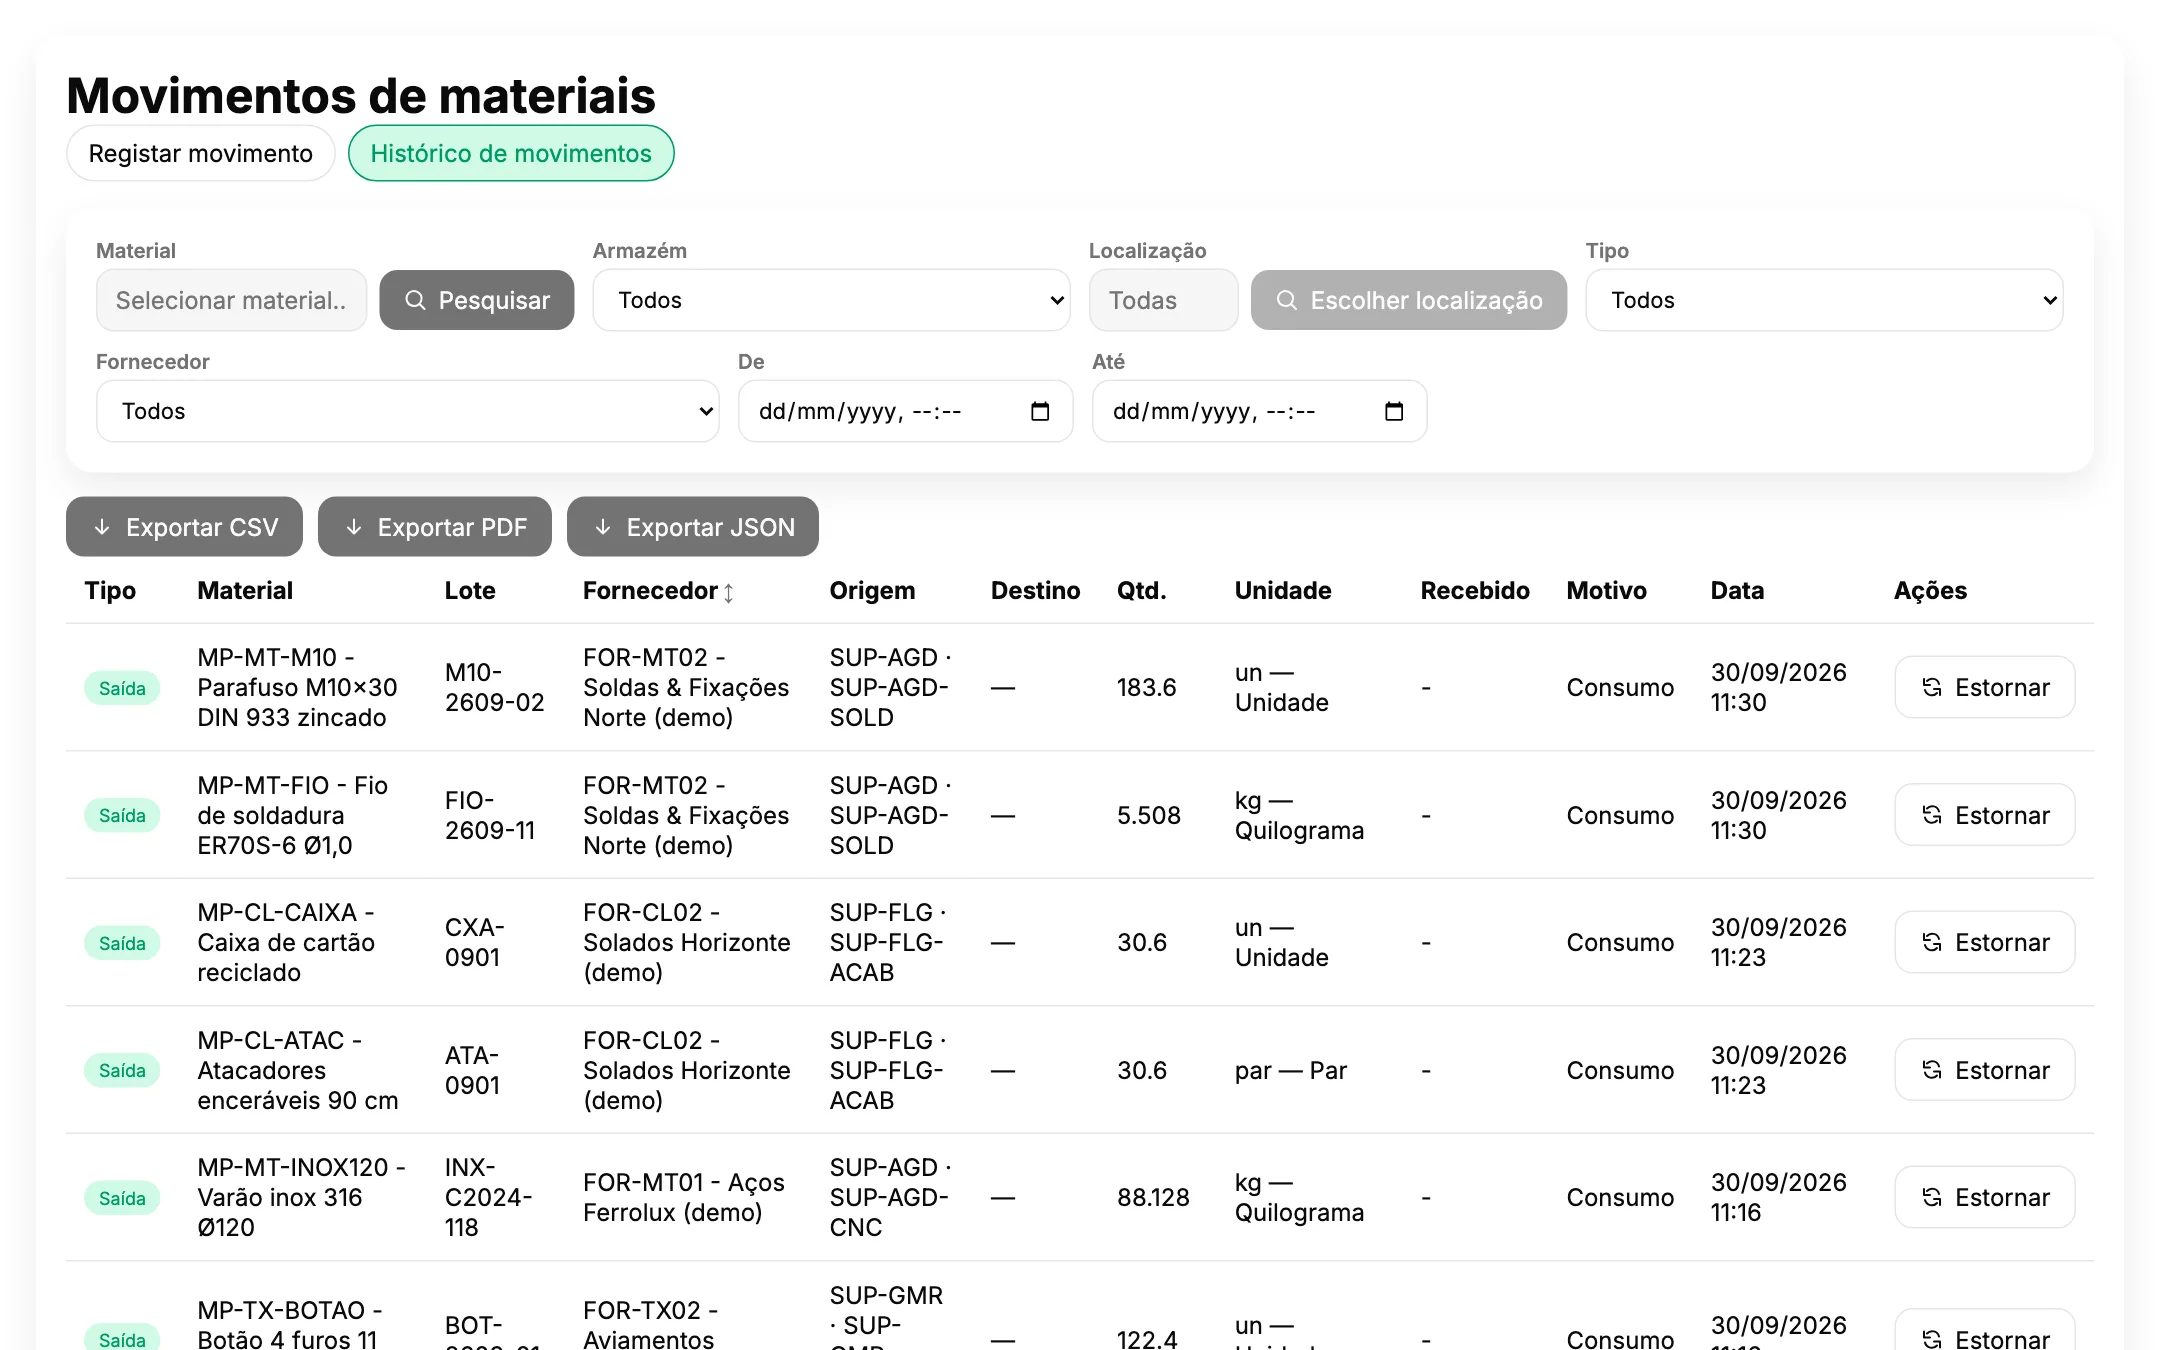
Stock by warehouse, location and lot, including the carts and containers at the line, with every receipt, transfer and consumption on record.
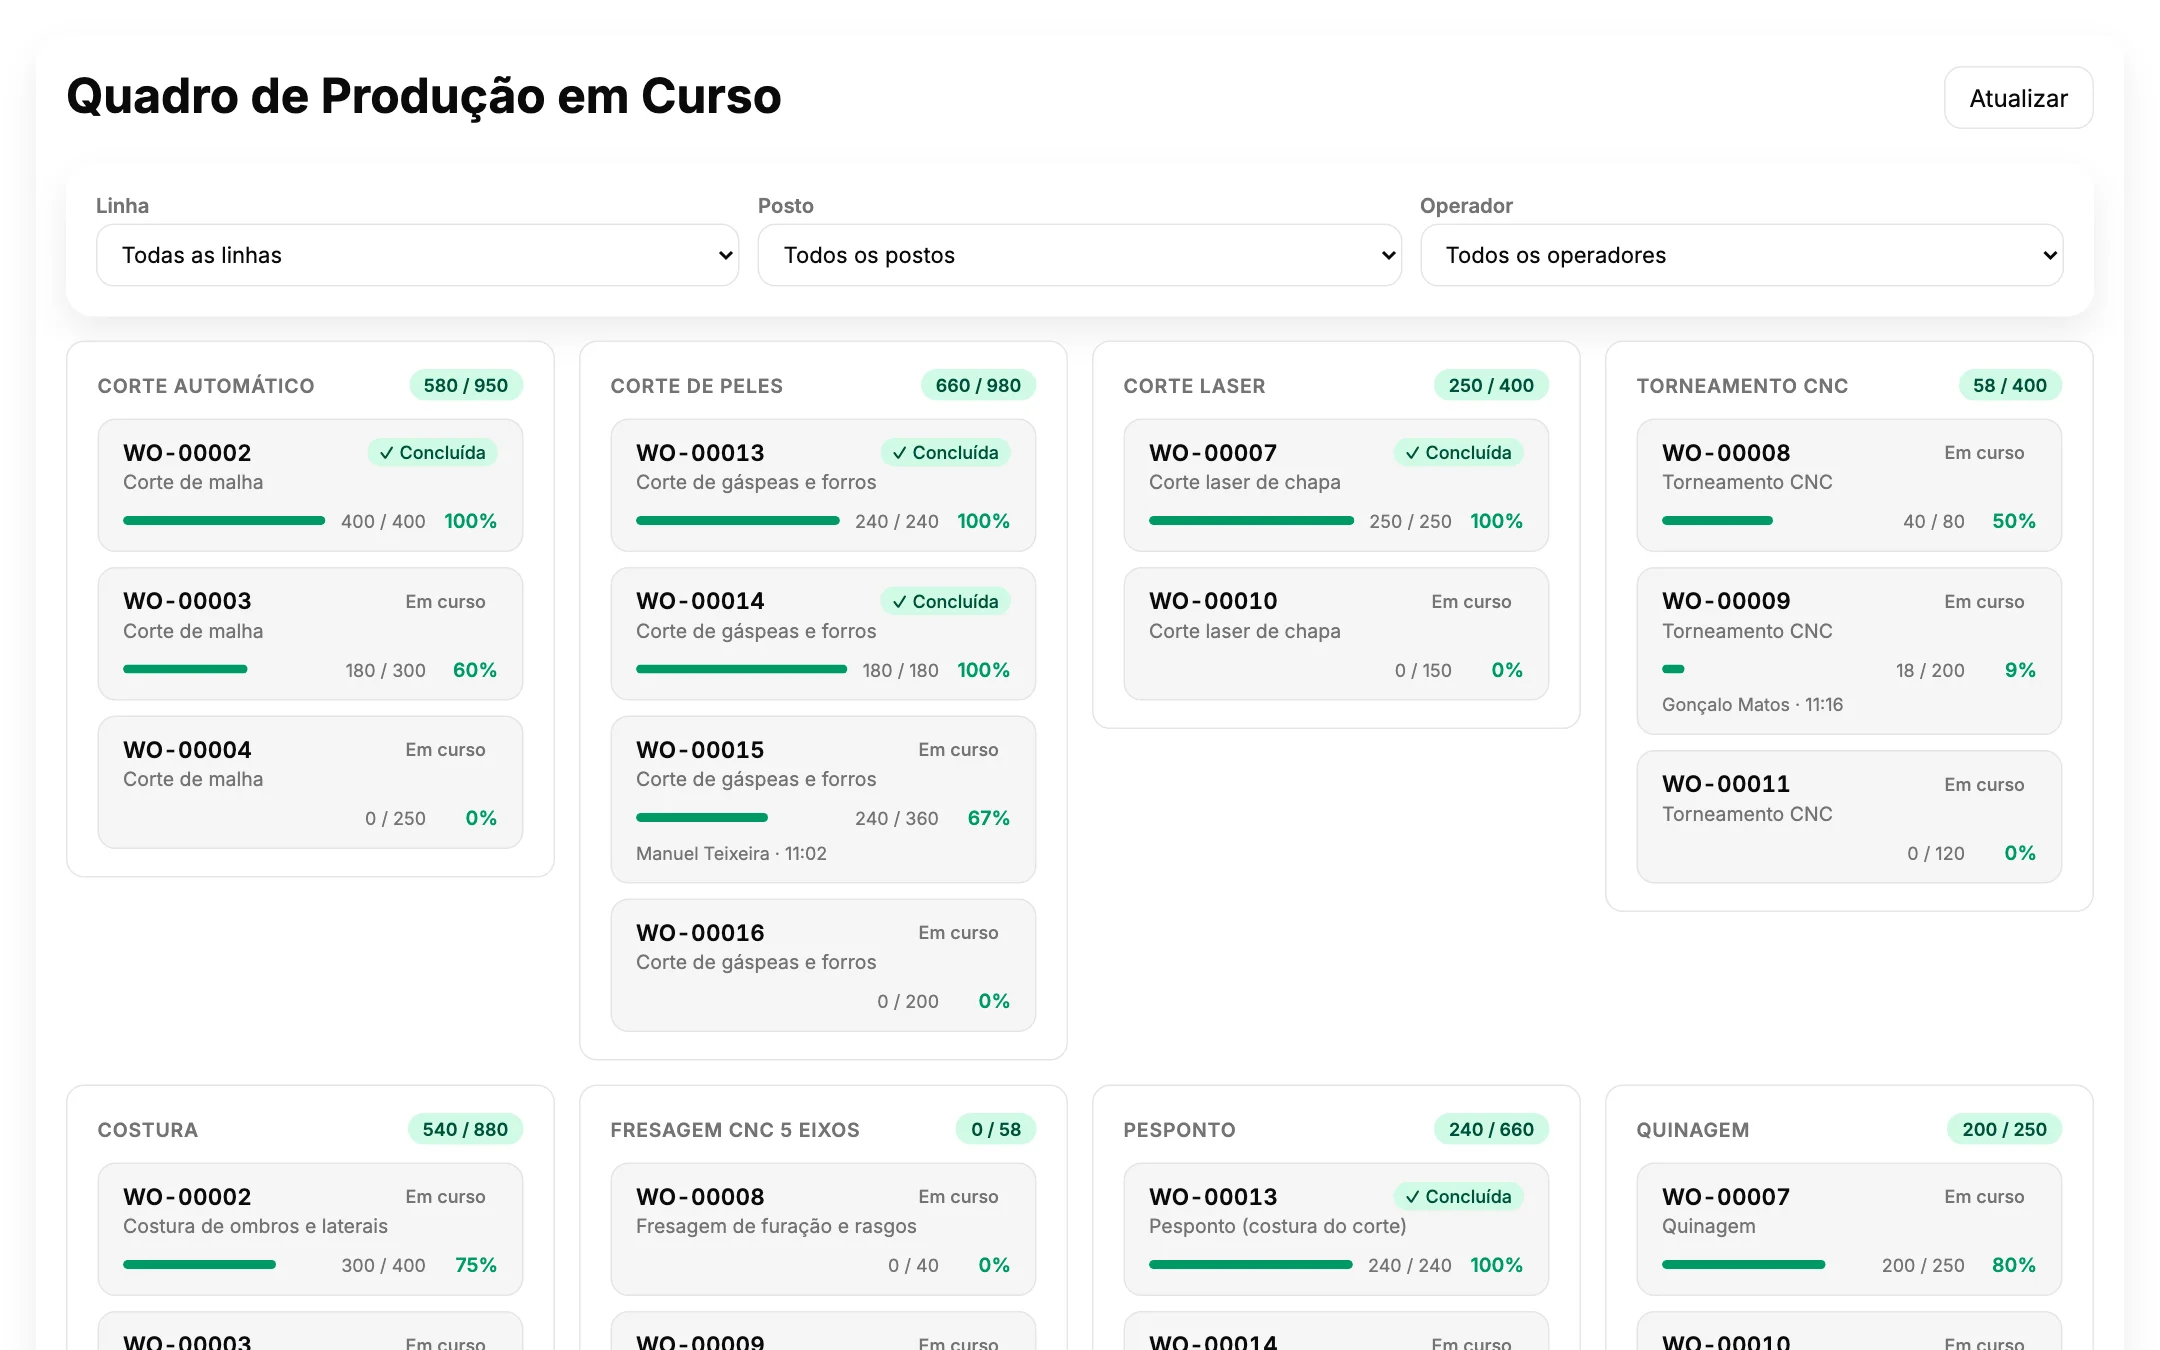
Production in real time
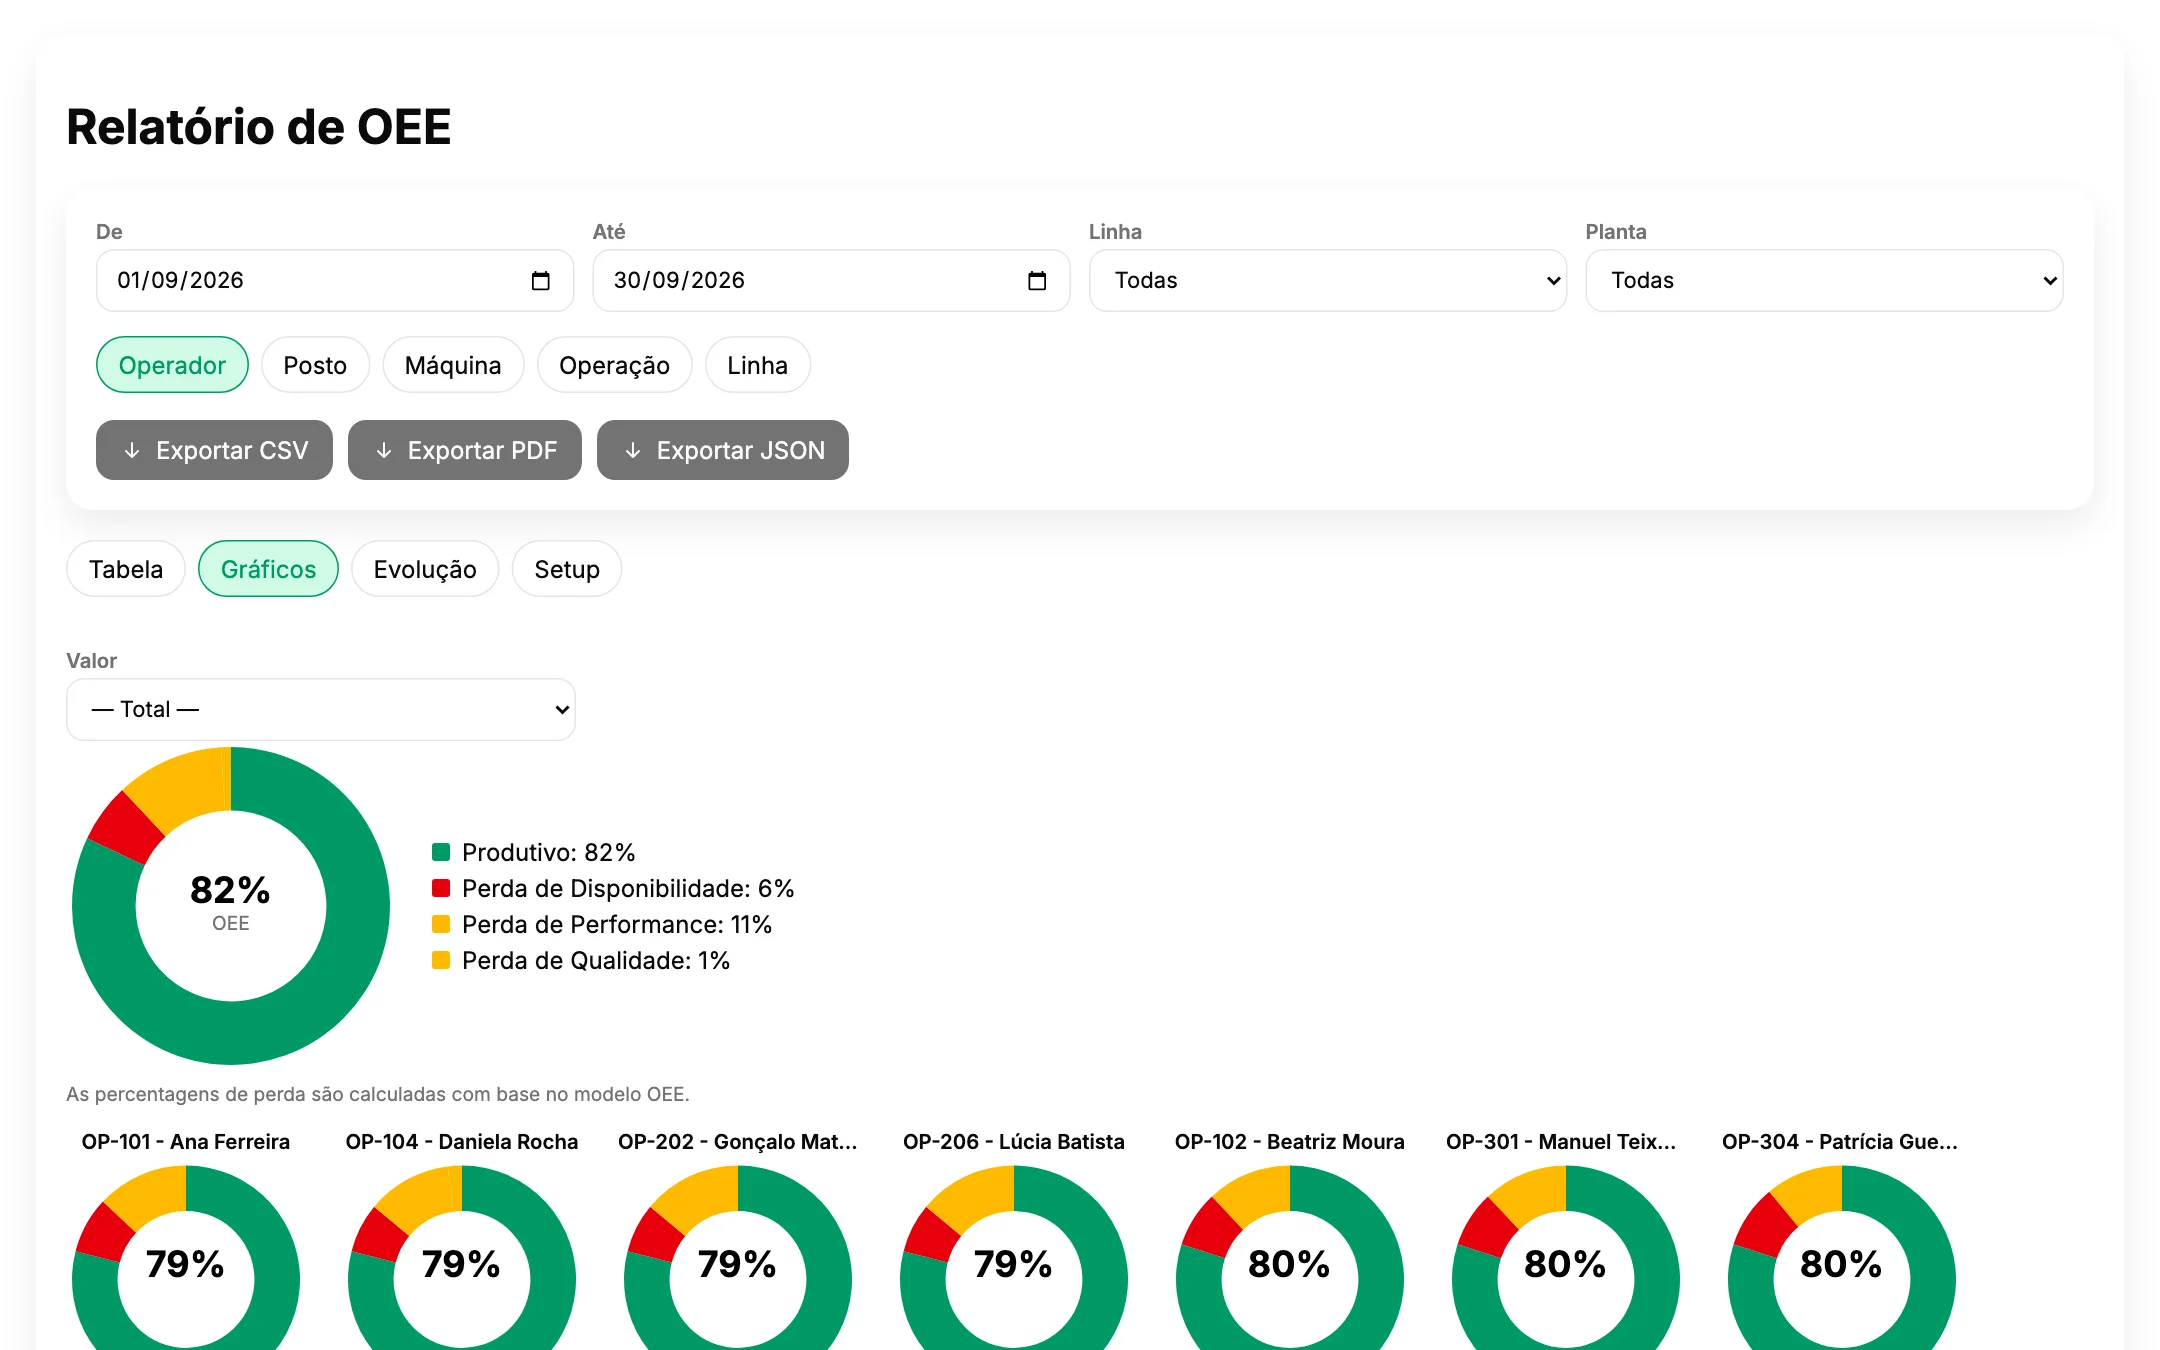
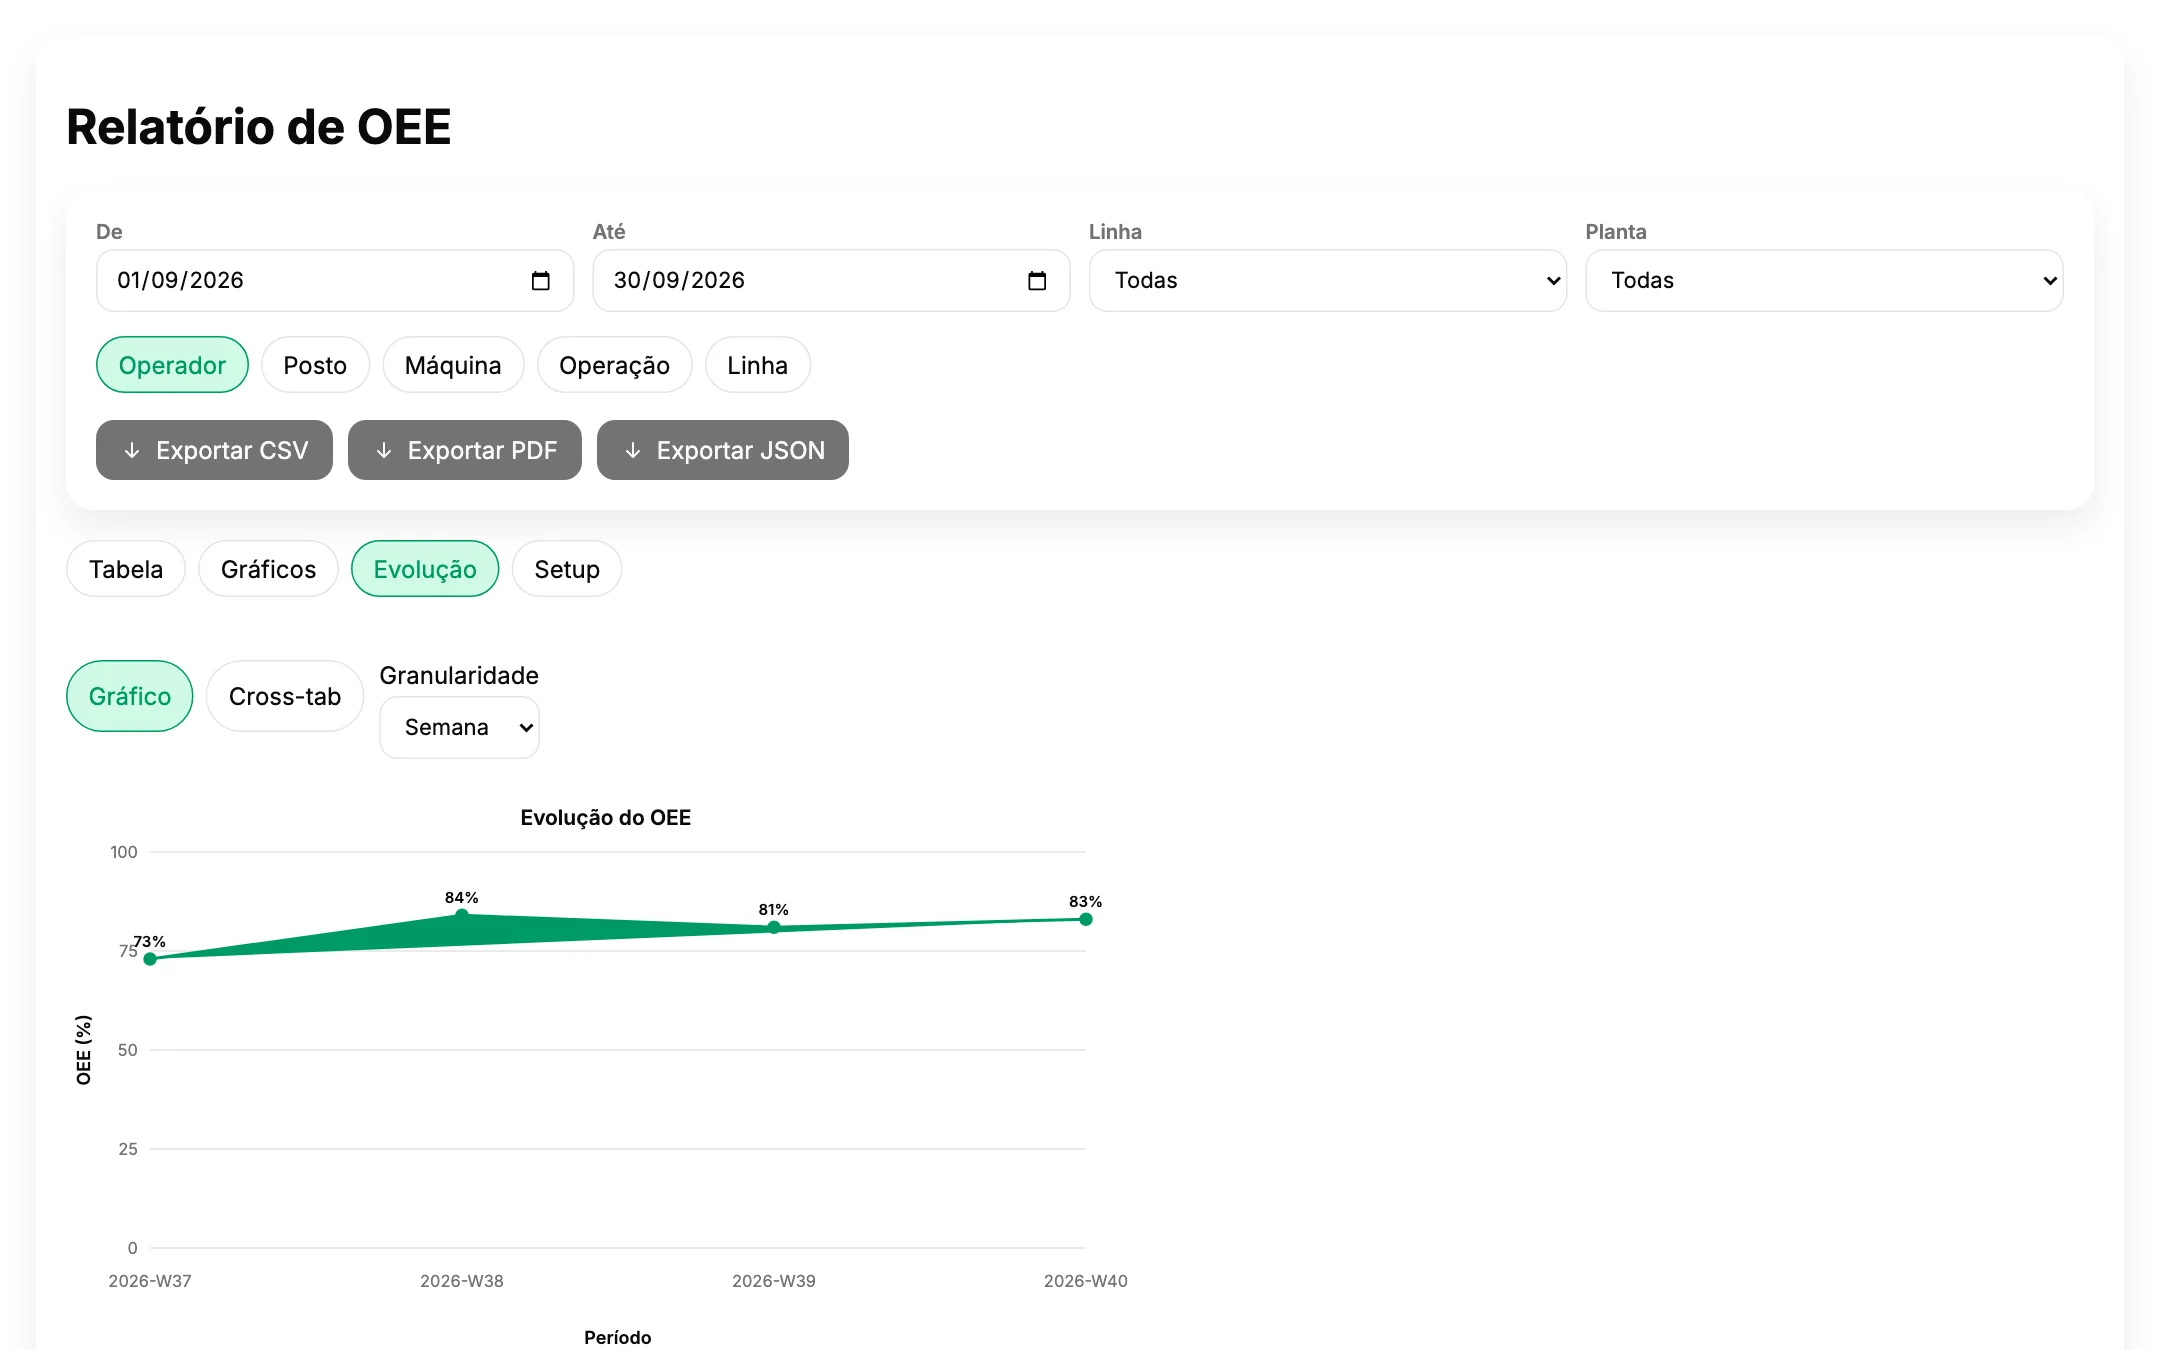
What each work centre is producing right now, and OEE calculated from the recorded events — by operator, station, machine, operation or line.
How it works
First we understand your floor. Then we adapt the solution.
The software is the proof, not the starting point. Every project follows the same three steps, and the first one happens where the work happens.
Requirements on the shop floor
We spend time at the lines and stations: how orders arrive, what is recorded today and where, where information gets lost. You get a written summary of what we found, whatever you decide next.
Adaptation to your process
We configure the solution around how you work — routings, stations, units, the words your people already use — and connect it to the ERP you run. Your process does not bend to fit the software.
Start-up, one area first
We go live on one line or one area, train the people who will use it every day and stay close in the first weeks, when the data shows recording habits before it shows production.
Serves your industry
Built on ISA-95, so it fits how your plant already works.
ISA-95 is the international standard for manufacturing operations. The model underneath is the same for any plant that turns materials into products — the examples below illustrate it, they do not limit it.
Textile and clothing
Knit cutting, sewing, quality check and packing, planned by size and colour, with trims requested to the sewing line.
Footwear
Upper cutting, stitching and finishing counted in pairs, with every lot of leather traced to the pairs it went into.
Metal, plastics and other processing
CNC turning and milling, laser cutting and welding, sequenced against the machines that set the pace, with bar and sheet stock by lot.
The same holds for processing in general: wherever there are orders, routings, work centres and materials, the model fits.
Start with your process, not with the software.
The first conversation is about how your floor works today, not a product demo. Then we tell you honestly whether this module, another path, or nothing at all is the right answer.